Lean Leadership Routines for Manufacturing Managers
Lean leadership is visible in how managers respond when work misses its expected condition. A useful routine takes the manager to the process, gives the people doing the work a clear way to describe the gap, and returns to check whether an agreed action helped. The purpose is to develop problem-solving at the source while making sure that safety, quality, delivery, and workload problems receive the support they need.
This guide helps a manufacturing supervisor build a manageable daily and weekly leadership routine. It covers what to observe, which questions to ask, how to assign follow-up, and how to improve the routine when it becomes a paperwork exercise. The example is illustrative; it does not report results from a named factory.
Define the work of a leader routine
A leader standard-work routine is a short, repeatable set of management activities connected to the work. It is not a checklist that proves a manager visited a department. It should help the leader see current conditions, respond to abnormalities, coach employees through a problem, and remove obstacles that exceed the team’s authority.
The Lean Enterprise Institute describes leader standard work through practices such as gemba walks, reflection meetings, response to Andon signals, accountability, and mentoring. These activities work together: a walk reveals a condition, reflection helps the team learn from it, and follow-up checks whether the response changed the work. A visit without listening or action does not create that loop.
Start with one production area and a small number of dependable routines. A supervisor who is responsible for a machining cell might review yesterday’s safety and quality abnormalities at shift start, observe one setup or handoff during the shift, and close the day by checking overdue actions. A plant manager might review repeated obstacles weekly and confirm that owners have authority and time to address them.
Build the routine around observed work
Before adding a form, spend time where the work happens. Ask operators and support staff what the expected condition is, how they know when it has changed, and what happens after they raise a concern. Compare the stated process with a real order moving through the area. Look for gaps between posted standards and actual work, unclear escalation paths, recurring shortages, work waiting for approval, and actions that remain open across shifts.
Choose a narrow purpose for the first routine. “Improve accountability” is not observable. “Review every open safety or quality abnormality at the start-of-shift board and assign an authorized response owner before the meeting ends” can be observed. State the affected process, trigger, owner, expected response time, and record that proves closure.
Keep the routine within the manager’s actual span of control. A supervisor can often correct a missing tool, clarify a work sequence, or request maintenance support. They may not have authority to approve a fixture redesign, change a customer specification, or release a capital purchase. The routine should make those boundaries explicit so that escalation moves the problem to someone who can act.
Use a short observation and coaching sequence
At the work area, the leader can use a consistent sequence without turning the conversation into an audit:
- Ask for the expected condition. “What should happen next, and what is the current standard?”
- Observe one instance. Follow a job, setup, inspection, or handoff. Do not infer the process from a summary board alone.
- Describe the gap neutrally. State what was expected and what was seen. Avoid labeling a person as the cause.
- Ask what the team has tried. Let the people closest to the work explain the condition and the evidence.
- Set the next test or escalation. Identify an owner, due time, guardrail, and the record needed to evaluate the result.
- Return to verify. Confirm whether the condition changed and whether the agreed method is practical across shifts.
Questions should open investigation rather than suggest an answer. Ask, “What changed between the last good part and this one?” before asking whether a particular tool is at fault. Ask, “Which records show that the material was available at the start of the job?” before concluding that the supplier caused a delay. If the team cannot see the process or retrieve the needed evidence, treat that as a system problem to solve.
Coaching does not mean withholding urgent support. Stop work and use the site’s safety or quality containment process when a hazard, suspect product, or uncontrolled condition appears. The leader can then coach the follow-up investigation after the immediate risk is contained.
Separate a signal from an action
A board metric is useful only when people know its definition and what response follows a miss. If “late jobs” means a different thing to production, planning, and shipping, a red square will create disagreement instead of learning. Define the measure, unit, time window, source, and accountable process owner before using it in a daily review.
Use one primary measure for the routine’s purpose and a few guardrails. For a setup improvement, the primary measure might be minutes from the last good part on the prior job to the first accepted part on the next job. Guardrails might include first-piece acceptance, safe lifting, and schedule adherence. Do not reward a faster setup if it shifts inspection work to the next department or increases defects.
When a measure misses its expected range, record the condition and the response. Do not change the target after seeing a disappointing result. If the definition or data source was wrong, document that defect and establish a corrected baseline before judging the countermeasure.
Illustrative example: repeated fixture search
Illustrative example — not observed plant performance. A supervisor notices that press operators sometimes leave the cell to find a fixture locator. The first response is not to demand that operators “be more organized.” The supervisor watches several job starts and asks the team to show the approved locator list, storage location, and return step.
The team finds that the current storage label uses an old fixture number and that a temporary locator has no marked home. The supervisor asks the toolroom owner to confirm the approved set, the operator representative to test a proposed location, and quality to confirm whether the identification will preserve traceability. The group records each job start where the locator is unavailable and each instance where a substitute is requested.
For one week, the team tests a labeled shadow location and a return check at job completion. Before the test, it agrees to stop if the location creates a trip hazard, obscures an inspection point, or causes an unapproved fixture to be used. The supervisor checks the first two starts per shift, asks operators whether the locator can be found without leaving the cell, and reviews any quality hold or safety observation.
At the review, the team compares the same records collected before and during the trial. If the search events fall but the new location is hard to maintain, the team adjusts the placement and repeats the check. If the records are incomplete, it does not claim improvement; it fixes the observation method first. The supervisor closes the action only after affected shifts have tested the location and the storage standard shows the current owner and revision.
Assign ownership and response expectations
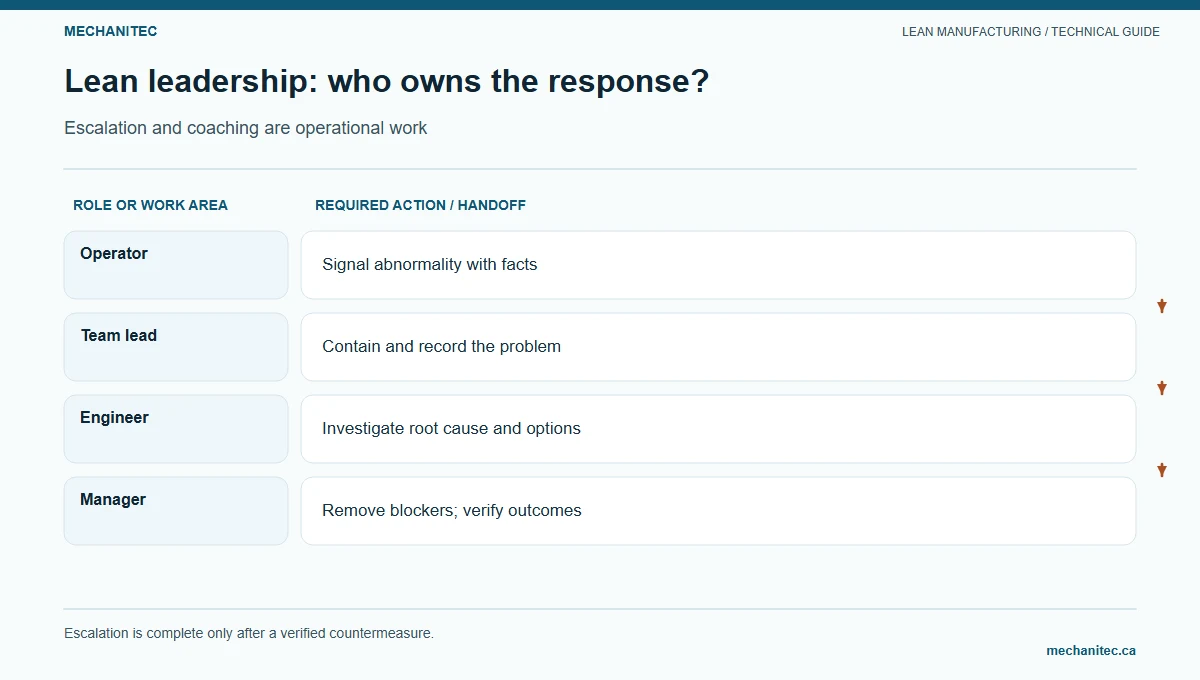
Use a simple role model. The employee who identifies the abnormality describes the condition and protects the work within their training. The process supervisor owns the immediate response and makes sure the issue is recorded. A technical owner investigates causes that require engineering, maintenance, quality, planning, or supplier support. The manager removes resource or policy barriers and decides when a problem needs escalation beyond the area.
| Signal | First response owner | Evidence to review | Escalate when |
|---|---|---|---|
| Safety hazard or near miss | Supervisor follows site safety procedure; employee stops or isolates work as trained | Location, task, condition, immediate control, and site incident record | Risk is not controlled or needs qualified EHS support |
| Suspect part or process drift | Production and quality contain affected work under the control plan | Part identification, inspection result, last known good condition, and traceability | Disposition, customer notification, or process change exceeds local authority |
| Equipment interruption | Operator calls maintenance through the defined request route | Asset, fault code or symptom, start time, response, and return-to-service check | Repeat failure or repair requires engineering, vendor, or capital decision |
| Missing material | Supervisor and material handler verify the signal and replenishment route | Part number, location, quantity, request time, delivery time, and shortage cause | Supplier, planning, or policy decision is needed |
| Overdue improvement action | Named action owner updates status and identifies the obstacle | Original due date, work completed, evidence, and next decision | Owner lacks time, authority, or cross-functional support |
Set response times by risk and operating need, not by a universal target. A hazard requires immediate control under the site’s safety procedures. A routine fixture-label change may be reviewed during the next shift meeting. A quality escape or customer-impacting delivery issue may require formal escalation. The board should show when the next response is due, not imply that every issue can be solved in the meeting.
Review the leadership routine itself
After two weeks, ask whether the routine helps people surface problems and obtain support. Check the work, not only completion rates. Are leaders visiting the process at the time problems occur? Do operators speak without fear of blame? Are actions closed with evidence, or merely marked done? Do the same issues return because the response addressed a symptom? Does the meeting take time away from production without producing a decision?
If the routine is too large, remove checks that do not lead to a response. If managers are filling out records after the fact, shorten the form and review why the work is difficult to capture. If actions repeatedly remain overdue, inspect workload and decision authority before adding reminders. A blank field can show that the routine is poorly designed, the activity did not occur, or the data was unavailable; it is a prompt to investigate rather than a reason to punish.
The Lean Enterprise Institute overview of leader standard work describes routines that include gemba walks, reflection, response to abnormalities, accountability, and mentoring. Use those practices to build a routine that supports your area’s work and its actual risks. For a related employee response loop, see how to manage employee improvement suggestions, and for shift communication see the shop-floor handoff guide.
Start with this weekly checklist
- Choose one process and name the leader accountable for the routine.
- Define the expected condition and the trigger that starts a response.
- Observe the work with the employees who perform and support it.
- Set one primary measure and safety, quality, delivery, or workload guardrails.
- Record the first response owner, next due time, and evidence required for closure.
- Escalate hazards, suspect product, and decisions outside local authority immediately through approved site procedures.
- Return to check whether the response changed the work across shifts.
- Review the routine after two weeks and remove steps that do not support a decision or learning.
The first measure to record is the number and age of open abnormalities within the chosen process, using one consistent definition. Pair that count with a review of a sample of closed actions: closure should mean the team checked a result, not only assigned a task. Keep the routine small, visible, and easy to improve.