Home » Choosing the Right Lean Tools: A Strategic Approach
Choosing Lean Tools by the Problem You Need to Solve
Contents
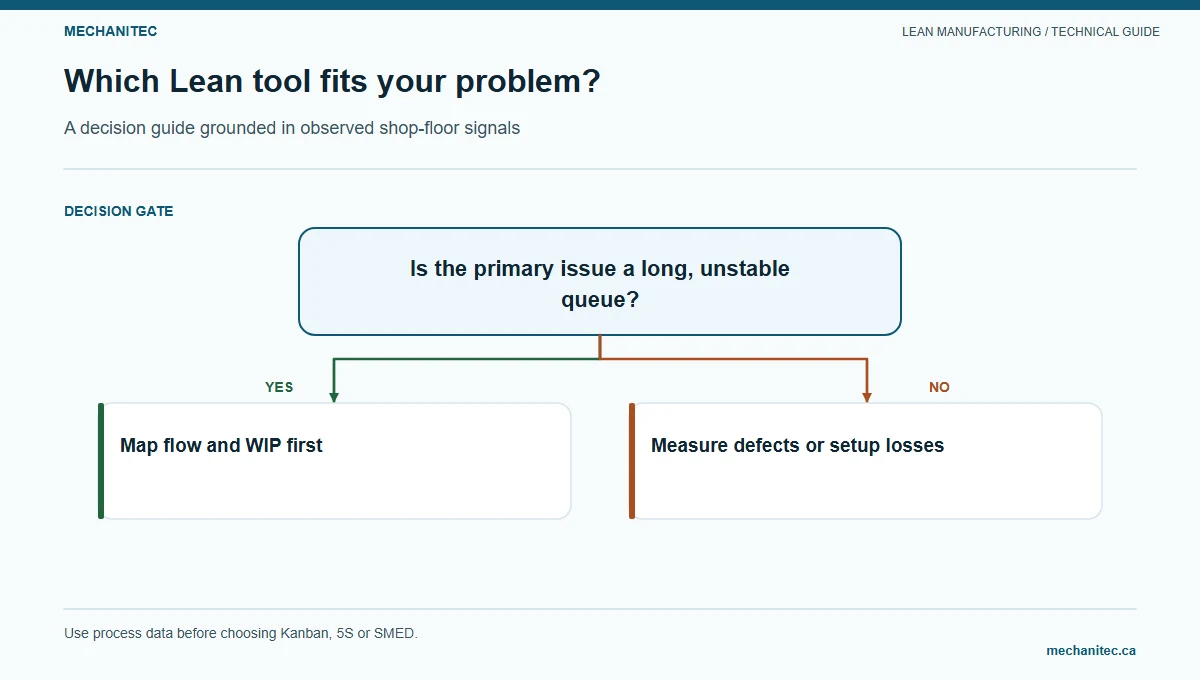
Choose a Lean method only after you define the observed problem, process boundary, and measure that should change. A tool name is not a diagnosis: 5S will not correct an unstable schedule, and Kanban will not fix an unreliable process or supplier by itself. Use this decision guide to select a first experiment, name its owner, and check for unintended effects.
A decision guide grounded in observed shop-floor signals. Mechanitec instructional diagram.
Start with an observable condition
Write one sentence with the work, the gap, and the evidence. For example: “Across the last 15 released orders in family A, the median wait between machining and inspection was 2.5 shifts; four orders waited because the inspection request was incomplete.” Separate observed facts from explanations. Confirm the pattern with operators and the records that define the process.
Before choosing a countermeasure, state the process boundary, sample window, shift or product family, and the current measure. Identify safety, customer, and quality requirements that the experiment must preserve.
Problem-to-method selection guide for a manufacturing team
Observed problem
Useful first method
Evidence to collect
Do not assume
Unknown waits and handoffs across a product route
Value-stream map one product family
Cycle time, queue time, changeovers, transfer batch, information release, and demand
A map alone removes waste or proves the future state is feasible
Repeated replenishment shortages at a stable use point
Moving tasks outside machine downtime is safe or valid without approval
A process varies and the cause is unclear
Use a problem-solving cycle; use statistical methods when the data support them
Operational definition, measurement system, time order, and subgroup conditions
A single average or short sample explains the variation
Check whether the method fits
Define the customer or next-operation need. Name the item, service, drawing revision, response, or delivery condition that must be met.
Walk the work. Observe the process where it happens and ask the people doing it to validate the sequence and exceptions.
Pick one measure. Define numerator, denominator, unit, time window, and data source. Add safety and quality guardrails.
Test the smallest reversible change. State the hypothesis, owner, start date, sample, approvals, and stop condition.
Review the evidence. Compare like conditions, record adverse effects, and decide whether to adopt, revise, or stop.
When evidence is missing, collect it before investing in software, equipment, or a plant-wide rollout. An improvement that moves a queue, adds inspection burden, or increases inventory may make one local measure look better while the full process worsens.
Connect the method to a real operating routine
Give the experiment one process owner and a review date. The owner checks whether the new method is followed, whether the expected measure changed, and whether safety or customer requirements remain satisfied. If the test succeeds under its stated conditions, update the approved work instructions and train affected shifts. If it fails, preserve the data and test the next verified cause.
Use this second pass after the first matrix narrows the options. The effort descriptions are relative planning guides, not cost estimates; the process owner must set labor, outage, software, and validation requirements for the actual site.
Detailed Lean method selection matrix; confirm local scope and approval
Method
Exact starting input
First success measure
Effort and owner
Key risk or precondition
Value-stream mapping
One product family, order-to-delivery boundary, observed material and information flow.
Lead time, queue, WIP, and handoff condition.
Cross-functional time; value-stream owner.
Map must reflect actual work and include customer demand.
5S
Bounded zone, approved tool/material positions, baseline search or abnormality data.
Search events, location misses, and actions verified.
Area team and supervisor.
Cannot substitute for guarding, safe-work procedures, or controlled storage.
Kanban
Measured consumption, lead-time range, pack size, supplier and quality status.
Shortage events, inventory, signal accuracy.
Materials, purchasing, and consuming area.
Needs reliable trigger, replenishment response, and exception handling.
SMED/setup analysis
Observed setup sequence, time definition, internal and external tasks.
Setup duration and good first-piece release.
Operators, maintenance, quality, engineering.
Do not move a task outside safe downtime without approved review.
Poka-Yoke
Failure mode, occurrence opportunity, escape and false-reject history.
Correct detection across challenge cases.
Quality and engineering design/validation.
Test reversed, missing, wrong, and device-fault states before release.
Jidoka/Andon
Abnormality trigger, response role, acknowledgement and escalation rule.
Missed call, response latency, repeat cause.
Cell team and support functions.
Support signaling remains distinct from engineered safety controls.
Standardized work
Approved sequence, current takt context, cycle and required standard stock.
Process stability, first-pass quality, and adherence to current method.
Operators, supervisor, process engineer.
Must be built with users and updated when the process changes.
OEE/loss analysis
Planned time, operating time, ideal cycle, total and accepted output.
Availability, Performance, Quality and verified loss minutes.
Operations and maintenance data owners.
Definitions and denominators must stay consistent; OEE is not a demand plan.
Root-cause/DMAIC study
Stable defect or delay definition and adequate, trustworthy sample.
Verified cause and sustained process result.
Process owner with quality/statistical support.
Weak measurement or small biased sample can invalidate a conclusion.
Daily huddle/leader routine
Current process measure, response roles, open actions, and escalation trigger.
Time to first response, overdue actions, recurrence.
Team lead and accountable manager.
Meeting activity is not improvement unless decisions return to the work.
Walk three scenarios before choosing
A welding jig is difficult to find
Record how often the jig is unavailable, search minutes, product families that use it, and whether the approved home remains convenient and safe. A bounded 5S change may fit if the jig exists but its location and return rule are unclear. If several jigs look alike or a wrong jig creates a quality risk, add positive identification and a controlled setup verification; visual organization alone will not prevent a mix-up. Kanban is a poor first choice when the problem is identity rather than replenishment of a consumed part. Verify the drawing or setup reference, preserve lifting and storage requirements, and check the next representative job.
The inspection queue is overfull
Measure arrivals and completions by inspection type, queue quantity, oldest-item age, staffing, and required hold or sampling rules. Check whether jobs arrive in large batches, documentation is incomplete, or one inspection method is the constraint. A value-stream map or focused queue study can clarify the flow; standard job readiness may remove avoidable waiting. Reducing inspection frequency without quality approval is the wrong method. A small test could improve the completeness of inspection requests, then compare queue age and first-pass documentation while holding acceptance criteria constant.
A bracket is repeatedly reversed
Confirm the failure mode, opportunities for error, current detection, escape history, and consequence. Error-proofing may fit if a fixture or geometry can prevent the wrong orientation, or an approved sensor can detect the specific condition. A poster or “be careful” instruction is a weak substitute when a physical control is feasible. Challenge-test correct, reversed, and missing-part conditions; measure correct detections and false rejects; include sensor failure and restart behavior. Quality and engineering must approve the design and validation before production use.
Set the test and stop conditions first
Write a short charter with the condition and baseline, suspected cause, chosen method, process owner, affected shifts, start and end dates, measure and source, required approvals, stop condition, and decision date. A stop condition could be a required control failing, a defect escaping, a shortage threatening an order, or a new safety concern. Identify who can stop the test and how the process returns to the prior approved state.
After the test, compare the same product scope and collection rule. Record whether the suspected cause was supported, what changed, any adverse effects, and whether the operators can explain the new response. If the result is inconclusive, improve the sample or measurement method before selecting a different tool. A method is ready to scale only when its inputs, control owner, abnormal response, and evidence of effectiveness are clear.
Respect method limits and distinct article roles
Lean tools are methods for understanding and improving work; none is a universal fix. A Kanban quantity cannot repair poor demand data. A 5S audit cannot replace a required safety inspection. A value-stream map is only as useful as the observed current flow. Standardized work should represent the best-known approved method and stay open to improvement rather than freezing an unsafe or ineffective process.
This page helps choose an approach. The dedicated VSM, Kanban, OEE, error-proofing, and 5S pages explain how to apply those methods. Use a contextual link when that guide provides the reader’s next practical step; do not repeat its detailed procedure here.
Build a baseline for six common shop problems
A manager can make a better selection when the team collects evidence from the actual job instead of asking which tool is popular. Use a short, representative sample and keep conditions comparable across shifts.
Six baseline checks to perform before selecting a Lean method
Problem signal
Sample and owner
Baseline to record
Question before intervention
Tool search
Observe repeated job starts; area lead records.
Search events and elapsed minutes by tool.
Does the tool exist, have an approved home, and fit current work?
Long setup
Time representative changes; operator and engineer observe.
Start, end, task sequence, first accepted piece.
Which tasks require the machine to be stopped and which require approval?
High scrap
Stratify several lots; quality owns definitions.
Defect count and total inspected by defect type.
Is the cause verified and can the measurement distinguish failure modes?
Growing WIP
Record queue by shift; production control validates.
Is a pull signal reliable and can supply replenish to the needed cadence?
Unbalanced work
Observe full cycles across products and shifts; process engineer owns.
Work content and cycle distribution at each step.
Does the mix permit rebalance without quality, ergonomic, or safety risk?
Choose a sample large enough to include normal exceptions, not only a clean demonstration. If the process changes by product, shift, or operator qualification, record that context. If measurement is unreliable, correct the collection method before deciding that the process itself is unstable. Do not combine unlike lots or redefine a defect after seeing the result.
Balance local improvement with the full process
A locally faster step can increase WIP, inspection burden, or rework downstream. Before changing a constraint, ask which step controls customer delivery and what the next operation can accept. A WIP limit needs a priority and replenishment rule; a faster machine may simply fill the queue more quickly. A new check may catch defects earlier but add workload; quality and engineering should evaluate whether it prevents escape and what reaction follows a failure.
Estimate effort with the people who will maintain the method. Include training, fixture or sensor validation, system configuration, document approval, supplier coordination, and audit needs. A low-cost visual label can still fail if there is no owner or replenishment route. A software dashboard can display more data without improving the response. Choose the smallest intervention that can test the suspected cause and preserve a safe rollback.
At the decision review, show the baseline, method, preconditions, expected measure, guardrails, assigned owner, and test result. Approve expansion only when the result repeats under representative conditions and the control plan is clear. If the method creates another queue, raises hidden cost, or requires an unapproved change, revise or stop it. This disciplined selection keeps tool use tied to customer need and shop-floor evidence.
Keep a decision log with the condition, evidence reviewed, methods considered, reason for selection, approval roles, and next review date. When a method is rejected, record the missing precondition or evidence needed to reconsider it. This makes the choice understandable to a new supervisor and prevents the team from restarting the same tool debate without learning from the prior test.
Review the matrix after a major product, supplier, or layout change. A method that fit yesterday’s demand or process may no longer meet today’s requirements.
Revisit the tool choice when evidence changes
Set a review date at the start of the experiment and state which new evidence would change the decision. A stable shortage may support a replenishment pilot, while a new supplier delay can invalidate the lead-time assumption. A queue may appear to be the constraint until timestamps show that incomplete documentation is the dominant wait. Keep rejected options and the reason for rejecting them in the decision record, then revisit the choice when product mix, demand, supplier performance, or process risk changes. This prevents the team from treating a selected tool as permanent policy after its original conditions disappear.