Home » Run a Lean Manufacturing Pilot from Baseline to Control
Run a Lean Manufacturing Pilot from Baseline to Control
Contents
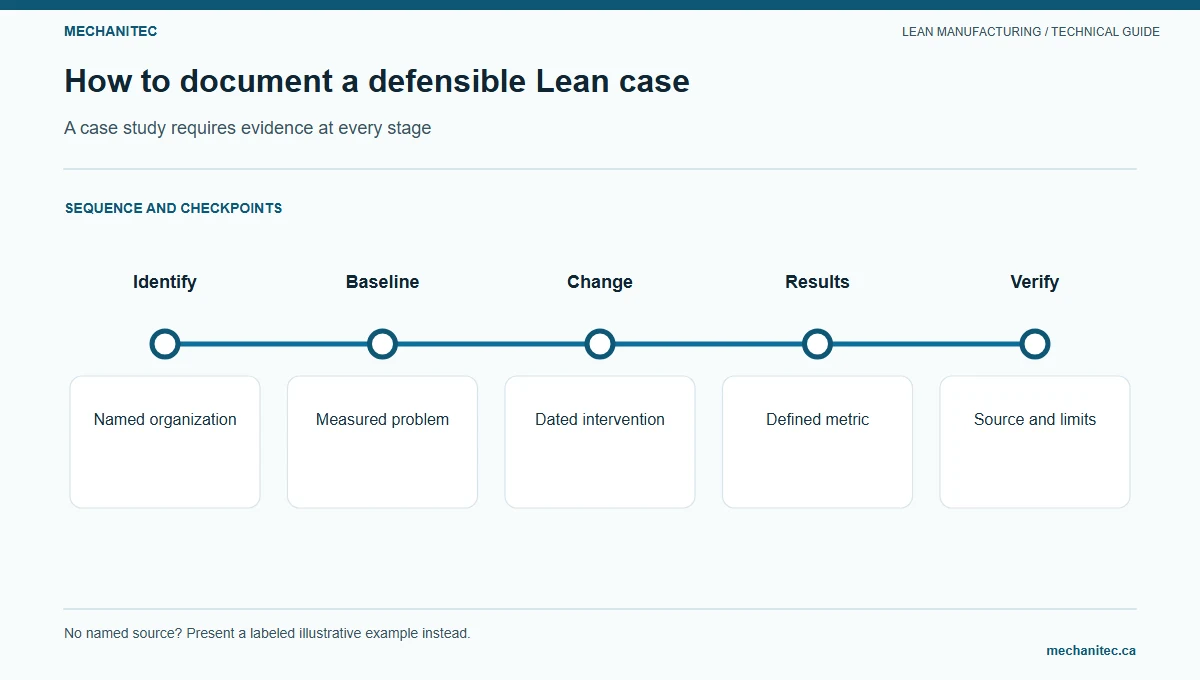
A Lean pilot is a bounded test of a specific process change. It starts with an observed problem and a defined baseline, protects safety and quality, and ends with a documented decision to keep, revise, stop, or extend the change. A pilot does not prove that a tool works everywhere. It shows whether a change improves this process under the conditions you measured.
Use this method when a product family has a visible constraint such as long queue time, excess work in process (WIP), repeated handling, setup loss, or avoidable rework. Choose one process boundary and one primary outcome. Keep the trial small enough to reverse if it harms safety, quality, delivery, or workload.
A Lean pilot moves from a defined problem to a controlled decision. Record evidence at each step.
Write a charter before choosing a Lean tool
A charter prevents a team from treating a tool as the goal. “Install Kanban” or “run a 5S event” describes an activity, not the process problem. Start with a measurable condition: for example, accepted orders wait several days between bending and welding, or operators repeatedly leave a cell to find approved fixtures.
Walk the process with the people who perform and support the work. Confirm the product family, route, shifts, order mix, inspection steps, and customer requirement. Agree on when the measurement starts and stops. If teams use different definitions, their before-and-after figures cannot be compared.
Copyable pilot charter
Field
What to record
Problem
Product or service family, observed condition, process location, and period observed.
Boundary
Start event, end event, included operations, shifts, and excluded work.
Baseline
Measure, unit, start and stop definitions, sample size, date range, and source record.
Aim
Expected change and review date. State it as a test target, not a promised result.
Guardrails
Safety, first-pass quality, delivery, traceability, ergonomics, and workload limits.
People and authority
Process owner, operators, maintenance, quality, planner, test lead, and approvers.
Decision rule
Evidence needed to keep, adjust, stop, or extend the change, plus the decision owner.
Set an aim that the team can influence within the pilot boundary. “Reduce average order-to-ship lead time” may be too broad if purchasing, outside processing, and customer approvals sit outside the trial. A narrower measure such as “reduce queue time from the completed bend operation to the start of welding” is easier to observe and act on.
Choose a measure that matches the problem
Separate flow measures from results and guardrails. Lead time is elapsed time between two defined events. Cycle time is the time required to complete a task or unit at an operation. Throughput is the number of conforming units completed in a stated interval. WIP is work that has entered the process but has not reached the chosen completion point. These measures answer different questions; do not substitute one for another.
Use a small set of measures:
Primary outcome: one result such as queue age, lead time, completed good units per shift, or setup duration.
Quality guardrail: first-pass yield, defects per unit, or rework hours, with the denominator stated.
Safety and workload guardrails: approved safety observations, ergonomic checks, overtime, staffing, or workload balance as relevant.
Context: product mix, order quantity, staffing, planned downtime, and unusual interruptions that could explain a change.
Define the data source before collecting data. Use travelers, machine records, inspection logs, dispatch timestamps, or a simple observation sheet. If timestamps are missing, record a sample prospectively. Do not reconstruct precise historical times from memory and present them as measured facts.
For a small sample, show individual observations or a median and range. An average can hide a few very long waits. For production counts, compare equivalent periods and distinguish good units from total starts. If work mix changes, report the mix and avoid a simple comparison that attributes every difference to the pilot.
Run the trial in controlled steps
Define the process family. Select parts that share a meaningful route and similar work content. List major variants, inspection requirements, and special approvals. If the parts do not share a stable process, narrow the scope.
Observe current work. Follow actual orders from the first boundary event to the last. Record queues, handoffs, travel, waiting reasons, rework loops, and changeovers. Ask operators what causes interruptions; verify each proposed cause at the process.
Establish a baseline. Collect enough observations to represent ordinary conditions across the selected shifts and mix. Record the exact measurement window and any exclusions. Preserve the raw sheet so another person can reproduce the summary.
Identify the constraint. Compare demand with available capacity by operation. Check whether the apparent bottleneck is persistent or caused by a temporary breakdown, missing material, or one unusual order. Do not move a queue without understanding why it formed.
Select one countermeasure. Link the change to the observed cause. Examples include a point-of-use fixture location, a standard replenishment signal, a revised work sequence, or a validated setup preparation step. Avoid changing layout, staffing, inspection, and scheduling at the same time if you need to know which change mattered.
Review hazards and approvals. Ask the safety, quality, maintenance, and engineering owners to review changes within their authority. Do not bypass guards, inspections, traceability, customer approvals, or validated process parameters to improve a speed measure.
Test and record. State the start date, responsible lead, affected shifts, training, temporary controls, and stop conditions. Record the same outcome and guardrails used for the baseline. Let operators report workarounds and unintended effects.
Review the evidence. Compare equivalent periods and work mix where possible. Report both the primary outcome and guardrails. Explain missing data and disruptions. A result that cannot be reproduced is a reason to extend or redesign the test, not to declare success.
Decide and control. The authorized process owner decides whether to stop, revise, sustain, or test a wider scope. If retained, update controlled instructions, training, replenishment rules, layout markings, inspection plans, and maintenance records as applicable.
A pilot is complete when the team can explain what changed, how it was measured, what happened to the guardrails, and who owns the process now. A workshop, new board, or rearranged cell is an activity; it is not evidence of a durable improvement by itself.
What a documented manufacturing case can teach
NIST’s Manufacturing Extension Partnership (MEP) published a case about Magline’s warehouse operations and cart shipping. The report says Magline contacted the Michigan Manufacturing Technology Center in July 2021. The work began with Lean training and a timed study; the reported time to locate and process one order was about 7 minutes 30 seconds. The team addressed order-to-product matching, labeling, shipping-area layout, product and people travel, and congestion at the parcel door.
NIST reports that equipment modifications were associated with $35,000 in cost savings, average time saved was 1.7 minutes per order (about 75 minutes per day), and travel time for completed orders to the dock fell by 30%. These are outcomes reported in the MEP case. The public summary does not provide the underlying order-level dataset, the full statistical method, or a controlled comparison, so readers should treat the figures as the case’s reported results rather than a universal forecast.
The transferable lesson is the sequence: observe a real process, time the work, identify specific matching and travel problems, adjust visual controls and layout, and measure the result. The case does not show that every manufacturer should add a door or spend the same amount. Magline’s warehouse context differs from a machining cell, and the report does not establish that the same intervention would improve every process.
For another example of primary-source reporting, NIST MEP describes a project at Current Applications in which employees used work-balance charts and smaller batches to improve flow. The report gives before-and-after production and WIP figures. Those figures belong to that company and its stated process; use the story to study the method, not as a target for your line.
Illustrative example: test a welding-cell constraint
Illustrative example — the figures below are invented for calculation practice. They do not describe observed plant performance.
A fictional fabrication shop has one shift with 420 planned production minutes after breaks and routine meetings. Customers require 100 accepted brackets each day. The demand takt is:
Available production time ÷ customer demand = 420 minutes ÷ 100 good brackets = 4.2 minutes per bracket.
A sample of comparable orders shows these average operation times: cutting 2.8 minutes, bending 3.9 minutes, welding 5.8 minutes, coating 3.1 minutes, and final inspection and pack 4.0 minutes per bracket. The welding operation is slower than the 4.2-minute takt. Its theoretical capacity at one unit per cycle is:
420 minutes ÷ 5.8 minutes per unit = 72.4 units per shift.
This calculation signals a capacity mismatch; it does not prove actual output, because breaks, downtime, staffing, yield, and product variation also matter. The team first checks whether the 5.8-minute observation includes interruptions or rework. It records the operation definition and samples several orders rather than relying on one timing.
Operators identify fixture loading and part repositioning as observable delays. The team tests a redesigned locator with engineering and safety approval. Before the change, the group records cycle time, first-pass yield, fixture-related near misses, overtime, and daily accepted output. During the test, it checks clamping, weld access, distortion, and the approved weld procedure. A shorter cycle is not accepted if the fixture makes weld quality or safe handling worse.
Suppose the follow-up sample measures welding at 4.4 minutes per unit. The theoretical capacity becomes 420 ÷ 4.4 = 95.5 units per shift. The station still does not meet a 100-unit demand on the same assumptions. The team should report the gap honestly, review the next constraint, and decide whether another controlled test is justified. It must not report “capacity increased to 100” or infer that customer demand was met.
Illustrative pilot record; use actual approved shop data before making a production decision
Measure
Before
Pilot
Interpretation
Weld cycle time
5.8 min/unit
4.4 min/unit
Sampled operation time; compare the same method and product family.
Theoretical station capacity
72.4 units/shift
95.5 units/shift
420 available minutes divided by cycle time; not actual good output.
First-pass yield
Record actual value
Record actual value
Good units without rework divided by units started.
Safety and workload
Record baseline
Record pilot
Stop or revise if a guardrail is breached.
Use a decision rule and a control plan
Before the trial, agree on what counts as a meaningful change and which guardrails cannot worsen. A team may require repeated observations across multiple shifts, no unapproved process changes, stable first-pass quality, and operator training before standardizing a new method. The acceptance rule should fit the process risk and customer requirements.
If the primary measure improves while quality, safety, delivery, or workload worsens, do not call the pilot successful. Contain the issue, involve the owner with authority, and revise or stop the change. If results are mixed, identify which product, shift, or operating condition differs. Averages alone may conceal a failure limited to one variant.
Once a change is approved, name an owner for each control. Define the measure, source, review interval, trigger, reaction, and escalation contact. A control plan should tell an operator or supervisor what to do when the process leaves its expected condition. A chart without a reaction plan will not sustain the improvement.
When to stop or redesign the pilot
The problem is outside the boundary. If most waiting comes from supplier shortages or customer approvals, a cell-level layout change will not solve it. Bring the responsible process owner into a broader study.
The sample is not comparable. A different product mix, shift length, staffing level, or outage can explain the apparent change. Collect a better-matched sample or report the limitation.
The countermeasure shifts waste. Lower WIP at one station may create expediting, overtime, or extra handling elsewhere. Follow the material to the defined process end.
A required control is weakened. Stop if the change bypasses an approved inspection, traceability, safety device, engineering approval, or customer requirement.
The process cannot maintain the new condition. If staffing, replenishment, calibration, maintenance, or training cannot support the method, revise the plan before expanding it.
For a broader rollout sequence, use the step-by-step Lean implementation guide. For flow diagnosis across multiple operations, see the value stream mapping guide. Lean Enterprise Institute describes standardized work as a current best-known sequence for completing work safely and consistently; use it as a baseline for improvement, not as a substitute for site-specific engineering controls.
Start the next pilot with this checklist
Name the product family and process owner.
Set measurable start and stop events.
Collect comparable baseline observations and keep the raw records.
Choose one cause-linked change and document its risk review.
Set safety, quality, delivery, and workload guardrails.
Review results with affected operators and authorized owners.
Record a keep, revise, stop, or extend decision and assign control ownership.
The first record to collect is the one that best describes the current problem: a timestamped order history, a repeated cycle-time sample, a WIP count, or a defect log. Let that evidence determine the next test.