Diagnose Lean Implementation Problems on the Factory Floor
A manufacturing Lean program can stall when shifting priorities and rework overwhelm the original plan. A team may hold daily meetings and post targets, but orders still arrive late, operators change sequences during the shift, and unresolved defects consume the time reserved for improvement. The right response is a plant-readiness review that shows which conditions block stable work and who can remove each barrier.
This guide helps a plant manager or improvement lead assess route stability, rework, equipment availability, training coverage, absenteeism, and backlog before restarting a Lean initiative. The example is illustrative and does not describe observed results from a named factory.
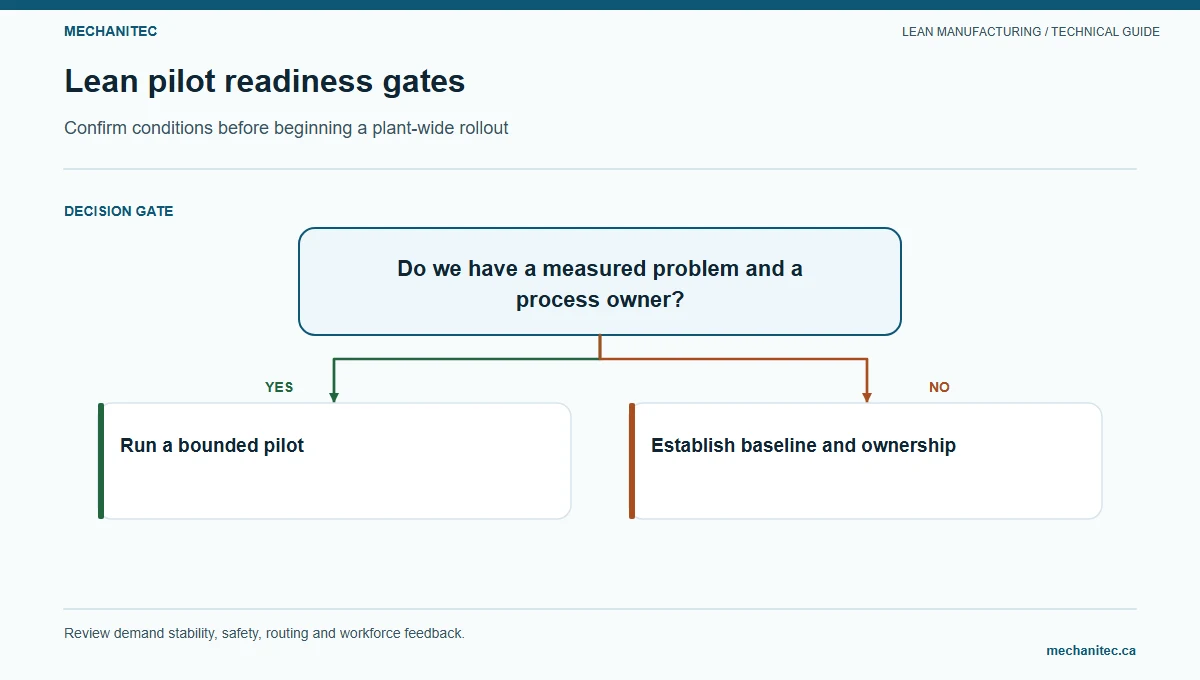
Define the stalled program as a process problem
Start with one product family or value stream. State what the customer needs, what the plant currently delivers, and which gap the team can influence. Avoid broad judgments such as “the culture is not ready.” A useful problem might be: “Released orders miss the planned weld start because material shortages and engineering changes alter the route after schedule release.” It identifies a customer consequence and a process to examine.
Set a fixed observation window, such as one representative production week. Include every affected shift and record the date, part family, route, constraint, and reason for changes. One week may reveal a problem; it may not represent seasonal demand or a longer maintenance cycle. Note those limits before making a decision.
Collect evidence from source records and direct observation. Review order releases and change logs for route instability; quality records and rework travelers for defects; machine logs for downtime; training matrices for qualification coverage; attendance data in approved aggregate form; and open-order lists for backlog age. Reconcile definitions with the people who maintain each record. A board count that cannot be traced is not a reliable baseline.
Use a 12-question readiness review
Score each condition as ready, needs action, or stop and contain. Add the evidence source, affected process, and person who can verify the rating. Do not average away a safety or quality blocker: one critical stop condition can prevent a trial even when other areas look ready.
- Can the team name the customer need and the product family within the proposed boundary?
- Does the released route match the current approved work sequence and revision?
- How often did the sequence or priority change after schedule release during the sample week?
- Are material shortages recorded by part, location, request time, and replenishment response?
- Can the team identify rework by defect, operation, product family, and disposition?
- Are current machine interruptions classified by cause and duration?
- Are critical jobs assigned to qualified people on all affected shifts?
- Can the team complete a change without unsafe overtime or missed required checks?
- Can employees see the current standard and report when actual work differs?
- Does the process owner have authority, time, and resources for the first test?
- Are quality, safety, traceability, and customer controls defined before the trial?
- Is there a scheduled review that can keep, revise, stop, or escalate the change?
A “needs action” rating should result in a named action, not a vague note. A “stop and contain” condition means the team follows the plant’s formal safety, quality, or customer process before improvement work continues.
Build a risk register from evidence
Prioritize barriers by risk to people, product conformity, customer delivery, and ability to run a valid trial. Include both impact and likelihood, but do not disguise mandatory controls inside a numerical score. The table below is a starting format; the plant should use its approved risk method where one exists.
| Barrier and evidence | Diagnostic check | Countermeasure | Owner and leading indicator |
|---|---|---|---|
| Route changes after release; schedule log shows repeated revisions | Compare released route with approved traveler and identify change source | Define release freeze point and urgent-change authority; resolve engineering dependencies | Planning and engineering; route changes after freeze per released order |
| Material arrives late; shortages cluster at weld start | Trace part request, inventory location, delivery time, and supplier or internal cause | Correct inventory records or test a replenishment signal after usage is stable | Materials owner; shortage events per released order |
| Rework repeats; defect codes or dispositions vary by shift | Audit samples against drawings, weld procedure, inspection plan, and rework records | Contain suspect work, standardize defect recording, and test one verified process change | Quality and weld engineer; repeat defects per defined opportunity |
| Machine availability is unreliable; interruption reasons are missing | Compare operator calls with maintenance work orders and downtime logs | Improve event coding, planned care, and response ownership before changing cell balance | Maintenance; unplanned downtime by verified cause |
| Training coverage is incomplete; current qualification matrix has gaps | Observe task performance against the approved skill requirements on each shift | Schedule qualification and trainer coverage before assigning new work | Production and training owner; qualified coverage by critical operation |
| Backlog age rises; jobs wait between operations | Sample order dates, queue entry/exit, priority changes, and customer need | Address the limiting handoff or release rule; do not push more work into the queue | Value-stream owner; queue age by operation and customer class |
Prioritize impact without hiding stop conditions
For routine barriers, a team can rate likely impact and frequency using its site scale. For example, a high-impact, frequent shortage in a critical route should receive earlier attention than a rare search for a noncritical tool. Record why the rating was assigned and who reviewed it. Do not use an arithmetic score to overrule a safety control, customer requirement, or nonconformance process.
Ask whether a barrier prevents safe work, makes measurements unreliable, or makes the process too unstable to test. If yes, fix or contain it before selecting a flow tool. When a barrier does not block a small trial, document how the team will control its effect. This keeps an improvement pilot from quietly depending on conditions that operators cannot reproduce.
Separate immediate control from long-term corrective action. A temporary material check may protect a scheduled job today; it does not correct the stock record or supplier handoff. Extra inspection may contain suspect product; it does not prove the weld process is capable. Give temporary actions an owner, expiration or review date, and exit condition.
Illustrative sample production week
Illustrative example — not observed plant performance. A metal-fabrication plant reviews one sample week for a welded frame family. It finds 18 released jobs, 5 route changes after release, 4 shortages recorded at weld start, 3 rework travelers, 2 machine interruptions without a coded cause, 1 uncovered qualification requirement on the evening shift, and 7 orders waiting more than one shift before the next operation. These numbers are invented for the example and should not be treated as a benchmark.
The team does not total these into a single “Lean readiness score.” It confirms that the missing evening qualification blocks the proposed weld-cell trial until qualified coverage exists. It also checks whether the 3 rework travelers represent one repeated defect or separate conditions. Planning and engineering review the 5 route changes to learn whether they came from customer priority, drawing revision, or missing order data. Materials traces the 4 shortages by part and source. Maintenance reviews the two uncoded interruptions against work orders and operator calls.
The team chooses only one initial intervention: verify current route and drawing revision before release for the frame family. Planning owns a revised check, engineering defines which changes require formal review, and the supervisor samples released orders on each shift. The leading indicator is the share of sampled orders with route and revision confirmed at release. Customer delivery, quality holds, and time spent correcting paperwork remain guardrails. The trial does not begin until the qualification gap is closed.
For example, if 16 of 20 sampled orders have the route and revision confirmed, the check is 80% for that sample (16 ÷ 20). That percentage is not a plant-wide result or proof that late orders will decline. The team should keep the numerator, denominator, date range, and sampling rule beside the value. If an order is changed after release, record the change and source rather than silently replacing the original route.
For backlog, report both the number of open jobs and their age by process step. An average age can hide a small number of customer-critical jobs that have waited much longer. A simple count by age band—same shift, one to two shifts, and more than two shifts—can support a daily review, provided the plant defines when the clock starts and pauses. Do not use a backlog chart to pressure employees to skip required checks or release incomplete work.
For machine interruptions, distinguish planned maintenance, setup, material wait, quality hold, and unplanned failure only when the records support those categories. If operators and maintenance use different event codes, reconcile the definitions before setting a target. A monthly uptime figure is not enough to decide whether maintenance or material flow is the constraint for a particular cell.
Use a first-30-day intervention sequence
| Period | Work | Owner | Review evidence |
|---|---|---|---|
| Days 1–5 | Define scope, gather records, observe all shifts, and contain safety or quality risks | Improvement lead with process, quality, and safety owners | Boundary, sample definition, open risks, and baseline quality |
| Days 6–10 | Score readiness questions and validate top causes with operators and support teams | Area supervisor and functional owners | Verified evidence, disagreement log, owner and due date for each blocker |
| Days 11–20 | Close blocking actions, then test one low-risk countermeasure | Named process owner | Leading indicator, primary result, guardrails, deviations and shift coverage |
| Days 21–30 | Review results, update controlled work if approved, and plan the next test | Value-stream owner with affected employees | After-action record, decision, training status, follow-up date |
If the test cannot start because a prerequisite remains open, the team should report that honestly and escalate the resource or authority issue. A delayed test with a clear blocker is more useful than an unapproved change with an unreliable result.
After-action review worksheet
At the end of a test, record the process boundary and period; the original condition and evidence; the countermeasure and its owner; actual participation by shift; the primary measure and guardrails; any deviations or unintended effects; and the decision. State whether the team will standardize, revise, extend, stop, or ask for a higher-level decision. List what evidence is still missing and who will obtain it.
Ask the operators whether the change is safe and practical, whether a workaround appeared, and whether they would use the revised standard on the next shift. Ask quality and maintenance whether the process remains controlled. Ask planning whether the change affects release or customer priorities. Close the review only when the decision, standard revision, training, and follow-up owner are clear.
Start the recovery with a clear decision
- Ready: prerequisites are controlled and a small test has an owner, measure, and stop rule.
- Prepare: the opportunity is valid, but a defined readiness action must close first.
- Pause: a safety, quality, traceability, staffing, or data gap makes a reliable test unsafe or invalid.
- Redirect: the proposed project does not address the observed customer or process problem; redefine the boundary.
For a general implementation sequence, use the Lean pilot roadmap. For a symptom-to-method diagnostic, see how to troubleshoot Lean tools. Keep this readiness review focused on whether the plant can run a safe, measurable test.
Your first step is to sample one production week and reconcile route changes, rework, downtime, training coverage, attendance, and backlog against source records. Give each measure a unit and owner. That review establishes which condition needs attention before the next improvement activity begins.
Protect the readiness review from becoming a meeting with no decisions. Share the evidence pack in advance, invite owners who can verify the data or remove a barrier, and finish with the next action, person responsible, and review date. Give employees time to correct the process description before management assigns a countermeasure.
Store the review with the current process record so the next shift can see what was decided and what is still unresolved.