Plan a Lean Manufacturing Transformation Around Real Work
A Lean transformation becomes credible when it connects a customer or production problem to observed work, a tested change, and a control plan. Training, new boards, and 5S activity can support the effort, but activity alone does not show that the value stream improved. Leaders need a sequence that begins with a verified condition and ends with a decision supported by measures and employee feedback.
This article uses a published NIST Manufacturing Extension Partnership (MEP) case to show how to read transformation evidence carefully. It then provides an illustrative staged method a manufacturer can adapt. The sample plan is not the history of the named company and does not claim that every factory should follow the same timeline.
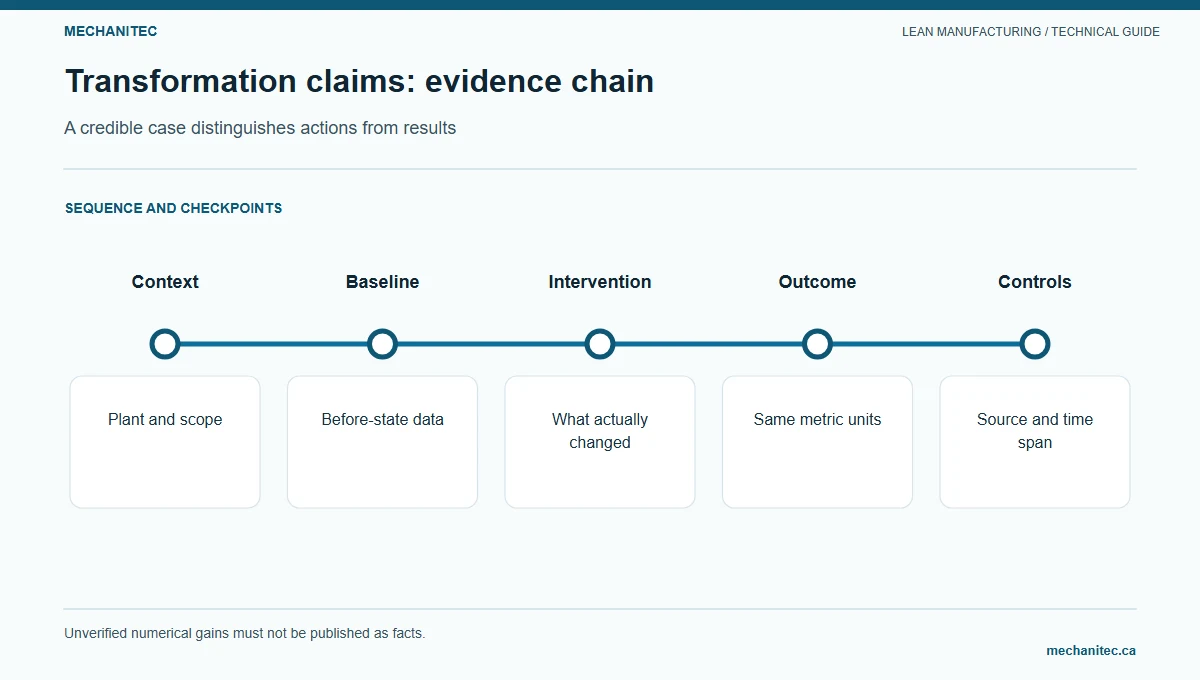
What the documented case supports
NIST MEP’s success story about Island Components Group describes a small manufacturer that sought to improve productivity within the limits of its workforce, processes, equipment, and floor space. With support from the Manufacturing & Technology Resource Consortium at Stony Brook University, the team received Lean training focused on just-in-time, Jidoka, and standard work. The reported work included one-piece flow, feeder-line Kanban, bottleneck management, and a plan-for-every-part template for material replenishment.
NIST reports that daily output increased from 75 to 120 units and work in process (WIP) decreased from 717 to 156 pieces. The arithmetic differences are 45 additional units per day and 561 fewer WIP pieces. Relative to the published starting values, output is 60% higher (45 ÷ 75), and WIP is about 78% lower (561 ÷ 717). Those percentages are calculations from the NIST figures, not additional results reported by the company.
The public story does not specify the full measurement window, product mix, calculation method, staffing, demand, or all balancing measures. It therefore supports those stated before-and-after figures in the published summary, but it does not establish that one tool alone caused the change, that the change persisted for a specified period, or that another manufacturer can expect the same result. The source should not be used to claim a specific transformation timeline.
| Claim used here | Source support | Known limit |
|---|---|---|
| The company worked within workforce, process, equipment, and space constraints | NIST MEP case description | Public summary does not give detailed capacity data for each constraint |
| Training addressed just-in-time, Jidoka, and standard work | NIST MEP description of training | Training duration and full curriculum are not specified on the page |
| One-piece flow and strategic bottleneck management were part of the overhaul | NIST MEP case narrative | Detailed before/after process map and intervention dates are not published |
| Daily output moved from 75 to 120 units | NIST MEP reported result | Denominator, product mix, observation window, and persistence are not stated |
| WIP moved from 717 to 156 pieces | NIST MEP reported result | WIP boundary and valuation are not stated; pieces are not days of supply |
| Kanban was used for feeder-line replenishment | NIST MEP case narrative | Card size, lead time, container quantity, and exception policy are not published |
Build the transformation around a value stream
Choose one product family with a clear customer need and an observable delivery or quality gap. Define the process start and finish, order types, shifts, demand period, and excluded steps. Include the functions that control the flow: production, planning, quality, maintenance, engineering, purchasing, material handling, and customer-facing roles where needed.
Follow actual jobs through the process. Record processing time, queue time, inventory, changeovers, defects, rework, schedule changes, information handoffs, and customer requirements. Use common definitions and trace a sample to source records. Note product mix and planned downtime. If orders follow different routes, map them separately or identify a representative family before calculating an average.
Use the current-state map to ask where the customer waits, what condition creates the delay, and which process owner can change it. Do not treat each Lean tool as a transformation milestone. A value-stream map can reveal a queue; it does not fix a missing schedule rule. A one-piece flow cell may reduce WIP for a stable family but could be unsuitable when demand is highly variable, equipment is unreliable, or safety constraints require a different layout.
Keep a transformation portfolio small enough to manage. List each opportunity, customer or process problem, expected learning, affected area, owner, required support, risk, and next decision. Rank work by the severity of the verified gap and the ability to test it safely. Do not launch more pilots than the organization can support with engineering, quality, maintenance, and frontline time.
For every pilot, name the accountable process owner and sponsor. The process owner controls the daily work and standard; the sponsor removes barriers and approves resources. An improvement lead can facilitate observations and data, but should not own a process that they cannot maintain after the project ends.
Set a gate before expanding a pilot. Confirm that the result is measured, guardrails remain acceptable, standard work is current, employees are qualified, and the next process can absorb the changed flow. If the pilot reduced WIP locally but increased shortages downstream, the value stream is not ready to scale. Extend or revise the test rather than multiplying the problem.
Use a staged transformation sequence
The phases below are an illustrative planning structure. They can overlap or take longer depending on risk, product mix, approvals, and available capacity. The plant should set its own review dates.
| Phase | Team work | Evidence to retain | Exit decision |
|---|---|---|---|
| 1. Define and observe | Select one family, confirm customer need, walk the route, reconcile baseline | Boundary, current-state map, source records, safety and quality risks | Is the problem specific and the baseline trustworthy? |
| 2. Stabilize prerequisites | Resolve revision, equipment, qualification, material, and containment gaps | Open-risk register, current standard, training and maintenance evidence | Can the team run a safe and repeatable test? |
| 3. Test one change | Run a bounded pilot with operators and cross-functional owners | Test plan, measure definitions, deviations, guardrails, results | Keep, adjust, stop, or extend the pilot? |
| 4. Confirm and standardize | Test across shifts, update controlled work, qualify affected roles | Approved revision, verification, audit method, training record | Can the process meet requirements repeatedly? |
| 5. Sustain and learn | Review performance, action age, recurrence, and adjacent constraints | Control plan, owner cadence, repeat-finding response, next problem | Maintain, improve, or re-scope the value stream? |
Illustrative factory sequence
Illustrative example — not observed plant performance. A job shop produces a family of welded equipment frames. The current route includes cutting, bending, welding, inspection, and shipment. Planners report changing priorities, operators report late material kits, and quality records show recurring fit-up rework. The team chooses the gap between material-kit readiness and the start of welding as its first study boundary.
During the observation period, the team follows representative orders and records kit-complete time, weld-start time, missing items, route changes, and fit-up defects. It confirms which kits were complete at the defined point and checks the part revision against each traveler. The first map shows that some “material delays” are actually incomplete work orders and some are shortages from a shared stock location.
The team does not immediately create a Kanban loop. Planning and engineering first define the release condition for a complete frame kit. Materials verifies stock accuracy for the recurring components. Quality and the weld engineer review the repeated fit-up defect under the approved nonconformance process. Operators from each shift help test a kit checklist and the storage location.
In a bounded pilot, the team tracks the share of released orders with a complete kit at the agreed point, elapsed time from kit-ready to weld-start, first-pass acceptance, shortage events, and labor spent correcting paperwork. It sets stop conditions for wrong revision, missing controlled inspection, unsafe lifting, or a quality escape. After the pilot, the team compares the same product family and definitions. If the measures are incomplete or the mix changed, it reports the limitation and repeats the test.
If the revised release and kit process is safe and repeatable, the process owner updates the controlled checklist, trains affected shifts, and sets a follow-up observation date. The next improvement may be a supplier signal or a weld-cell layout change, but the team chooses it only after reviewing the new constraint. It does not assume that every item should use the same replenishment method.
Choose measures that show both flow and control
Select a primary outcome tied to the customer or process problem, such as order-to-ship lead time, queue age at the constraint, schedule attainment, or first-pass acceptance. Define the numerator, denominator, start and stop events, product family, time window, and data owner. Add guardrails for safety, quality, delivery, workload, traceability, and environmental controls as relevant.
Separate flow measures from activity measures. Number of workshops, trained employees, mapped processes, or suggestions can show participation but not customer value by itself. A WIP count should include a process boundary and unit; pieces are not interchangeable with days of supply unless demand and unit definitions support that conversion.
Use a before/after ledger for each measure:
- Measure name, unit, and exact definition.
- Product family, process boundary, and shifts included.
- Before and after values, sample size, and date range.
- Source record and person responsible for extraction.
- Demand mix, staffing, equipment, or policy changes that affect comparison.
- Guardrail results and any adverse or unintended effect.
- Whether the result persisted at a scheduled follow-up.
When public case data lacks a measurement window or denominator, say so. Do not use a claimed improvement percentage as a target for a different factory. The NIST example offers reported output and WIP values, while the measurement context remains limited in the public summary.
Make training and leadership part of daily work
Train employees on the specific process and problem-solving method they need for the pilot. A classroom explanation should be paired with practice at the work area, feedback from a qualified trainer, and a record that confirms task capability where required. Operators should help revise standards because they see normal variation and workarounds that a project team may miss.
Leaders should review the process, respond to abnormalities, provide time for experiments, and remove barriers that exceed local authority. A daily board should show the expected condition, the observed gap, owner, next action, and due time. It should not become a scoreboard for blaming employees. For leadership practices, see the Lean leadership routine guide.
When a trial changes work, supervisors need to confirm that all shifts can follow the approved method. If a shift lacks training or equipment, do not declare the new standard stable. If temporary staffing or overtime carries the pilot, report it as a condition and decide whether the process is sustainable at normal staffing.
Review the management cadence as the transformation grows. Daily area reviews should resolve local abnormalities; weekly value-stream reviews should address cross-functional dependencies; periodic sponsor reviews should decide on staffing, investment, and priority conflicts. Keep each meeting tied to a decision and a defined record so the same issue is not repeatedly escalated without new evidence.
When an improvement affects suppliers, maintenance, or customer approvals, include those dependencies in the schedule and risk register. Do not interpret a missed milestone as poor execution until the team checks whether the required decision, resource, or input was available.
Keep an after-action record for each stage. Capture what the team expected, what it observed, which assumption changed, and what the next stage will test. This prevents the transformation plan from becoming a fixed calendar that ignores what the work has taught the team.
Use a reproducibility check before claiming success
- Can another analyst identify the same orders and reproduce the baseline?
- Are units, denominators, dates, boundary, and exclusions documented?
- Do both periods cover comparable demand mix and shifts?
- Can source records confirm the output, WIP, defects, safety, and delivery values?
- Did the team preserve required controls and report deviations?
- Did employees across shifts test and accept the current standard?
- Did a follow-up check confirm the result persisted?
- Are limitations and alternative explanations stated clearly?
If the answer is no, describe the finding as preliminary and identify the missing evidence. A transformation should build the ability to observe, test, and sustain changes. It should not depend on a dramatic percentage that cannot be reproduced.
For a practical pilot charter and control plan, see the Lean manufacturing pilot guide. For documented production and WIP figures, read the NIST MEP Island Components Group case. Its public report supports the specific figures described above, with the stated limits.
Your first action is to choose one product family and reconcile one representative week of route, queue, quality, and WIP records. Once the boundary and definitions are stable, the team can select a pilot that addresses a verified constraint.