Home » Build a Manufacturing Improvement System That Closes the Loop
Build a Manufacturing Improvement System That Closes the Loop
Contents
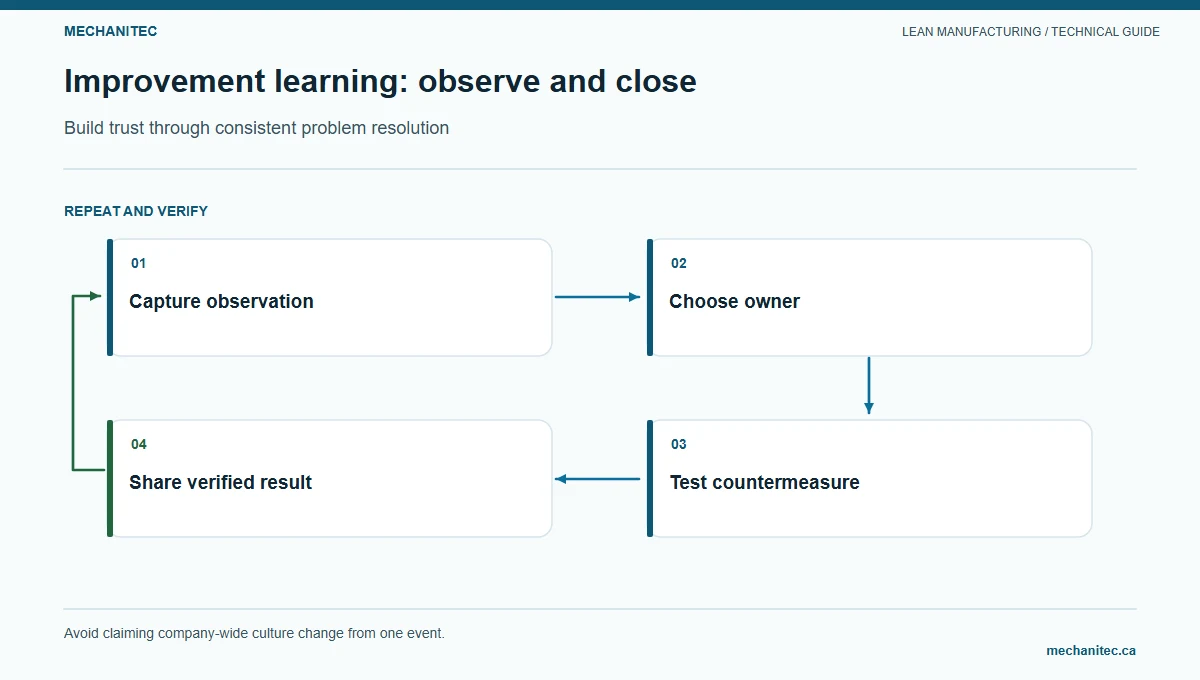
A manufacturing culture of improvement shows up in what happens after an employee reports a problem. The concern is acknowledged, the right owner reviews it, a safe response is chosen, and the employee learns what happened. Posters and suggestion boxes cannot create that cycle by themselves. Teams need a reliable route from observation to decision and follow-up.
This guide describes how to build an employee improvement response system for a factory. It covers intake, risk review, ownership, response targets, trial controls, and feedback. The ComDel Innovation example below is limited to the facts published by NIST MEP; the workflow and examples in this article are practical guidance, not a report of ComDel’s internal suggestion process.
Improvement participation grows when each report receives a clear review and response.
Separate participation from idea counts
A high suggestion count does not prove that employees can influence work. A low count does not prove that they are disengaged. Counts can change with staffing, production mix, training, reporting effort, or management attention. Pair participation measures with response quality: how quickly concerns receive an acknowledgement, how many have an owner, how long decisions take, and whether the person who raised the issue receives an outcome.
Use a clear definition for an “improvement idea.” It can be a concern, proposed experiment, safety observation, quality issue, maintenance request, or a change to a standard. These categories may need different routes. A suggestion form should never delay a safety report, nonconformance notice, near-miss report, or customer escalation required by site procedure.
Keep the first system simple. An employee should be able to record what they observed, where and when it happened, who or what work it affects, and whether an immediate risk exists. The employee does not need to write a root-cause analysis or design the final fix before submitting. Those steps can discourage useful observations and transfer technical responsibility to someone without the authority to make the change.
What a documented case can and cannot show
NIST MEP’s ComDel Innovation success story describes a manufacturer in Wahpeton, North Dakota, with 330 employees across plastic injection molding, automated assembly, tooling, precision machining, and other services. ComDel sought Lean training for newer employees as its customers, workforce, and product mix grew. Impact Dakota provided three Lean 101 sessions to a cross-functional group of 50 people from production, supply chain, process engineering, and quality. NIST reports that participants applied the concepts in their work areas and scale-up projects, that daily improvement ideas increased, and that ComDel held additional training for production technicians.
The published case does not report a baseline idea count, a measurement window, a response-time measure, or a controlled comparison. It supports the practical point that cross-functional training was used to build shared Lean knowledge and that the company reported more daily improvement ideas. It does not establish that training alone caused a quantified culture change, nor does it disclose ComDel’s internal idea-tracking process. Do not assign a percentage or promise similar results from this example.
For a smaller plant, the transferable question is operational: after people learn to identify waste and test a change, can they raise an idea, get the right decision, and see whether the change worked? Training supplies vocabulary and practice. The response system determines whether the observation becomes learning or disappears into an inbox.
Design an improvement intake route
Choose a route people can access during work: a board near the process, a short digital form, a supervisor conversation recorded on a standard card, or a combination. The route should work on every shift and for employees who do not use a computer during production. State who checks submissions, how often, and what to do when an immediate safety or quality issue arises.
Ask for only the information needed to route and investigate:
Location, process, shift, and date of observation.
What happened, including the expected condition if it is known.
Effect on the operator, next process, product, customer, safety, quality, or environment.
Whether work is stopped, contained, or still at risk.
Optional suggested change, with space to say “I am not sure.”
Name or contact route for follow-up; allow anonymous submission only if policy supports it.
Do not ask the reporter to estimate financial savings or prove a root cause. A safety hazard may be important without a cost calculation, and an employee may see a repeat defect before the process data is organized. The responsible technical owner should verify the condition and any benefit claim.
Triage by risk and decision authority
Review each submission for urgency first. A hazard or suspect product follows the site’s established safety or quality path. A process concern that does not require immediate containment can enter the normal improvement queue. The triage owner should label what happens next, who owns it, and when the reporter can expect an update.
Improvement intake and response roles
Submission type
Immediate route
Decision owner
Feedback to reporter
Safety hazard or near miss
Use site safety reporting and stop-work controls as trained
Supervisor with EHS support
Confirm immediate control and next review under site procedure
Suspected defect or traceability concern
Contain and notify quality through the formal nonconformance route
Quality and process owner
State disposition or investigation status without exposing restricted information
Equipment issue
Request maintenance support and follow lockout requirements
Maintenance owner and area supervisor
Report priority, repair status, and any change to the standard
Small process improvement
Log the idea and confirm process boundary
Area owner with affected employees
Accept for test, request evidence, defer with reason, or explain why it is outside scope
Cross-functional or capital change
Record dependency and route to authorized review
Manager, engineering, finance, EHS, or other required approver
Give a decision date and identify missing information or constraints
Response targets should reflect risk and capacity. A plant can set an acknowledgement within one working day and a triage decision within a few working days, but these are local targets to adjust to staffing and urgency. Any urgent issue follows the shorter formal response already required by the site’s safety or quality system. Do not create a parallel rule that conflicts with a regulated or customer-controlled process.
Test ideas with the people who do the work
For a low-risk change, frame the test before implementation. Define the process boundary, expected condition, current measure, proposed change, duration, owner, affected shifts, and stop rule. Ask operators what could fail and whether the change is usable under real production conditions. Include quality, maintenance, engineering, planning, or EHS when the change touches their controls.
A test should be small enough to reverse and long enough to expose normal variation. Record the result using the same definition before and after. If a change affects a controlled document, machine setting, inspection method, or customer requirement, use the required approval and revision process before making it live.
When the test does not work, explain what the team learned. The idea may have addressed a symptom, depended on a condition that was not present, or moved work to another step. Record the next question. Do not leave the reporter with “rejected” and no reason; a clear explanation helps employees understand constraints and improve future suggestions.
Illustrative example — not observed plant performance. An operator reports that two fixture clamps are often missing at the start of a welding job. The operator also says the current shadow board is hard to read from the work position. The supervisor acknowledges the report, checks whether any job is currently at risk, and records the part families and shifts where the issue occurs.
The area owner observes several job starts with operators from both shifts. They confirm the clamps have two similar labels and that an approved spare is stored outside the cell. Quality confirms the clamps are not part of a controlled inspection fixture; EHS checks the proposed storage location for access and reach. The team sets a two-week test of new labels and a point-of-use location, with a rule to stop if the location blocks an aisle or causes an incorrect clamp to be selected.
The process owner tracks missing-clamp events per job start, time spent searching, first-pass quality, and any safety observation. One operator tests the labels, another verifies them on the next shift, and the supervisor returns after each shift handoff. If the count falls but an unapproved substitute appears, the team stops and corrects identification before continuing. At the review, the reporter hears which change was accepted and what evidence supported the decision. The controlled storage standard changes only after the process owner confirms it.
This response creates a complete loop: observation, acknowledgement, verification, safe test, review, and feedback. It does not require the employee to own a technical change or guarantee a particular savings amount.
Track whether the system responds
Use a small set of measures that help leaders find a stuck point:
Submissions received by type and area, shown as counts rather than performance rankings.
Time from receipt to acknowledgement and to triage decision.
Open items by age, owner, and reason for delay.
Share of closed items with a recorded outcome communicated to the reporter.
Repeat issues and items reopened after an ineffective change.
For tested changes, the primary process measure plus safety, quality, delivery, and workload guardrails.
Interpret these measures carefully. A rise in submissions can mean people trust the route, an underlying process has worsened, or a reporting campaign increased awareness. A decline may mean fewer issues, limited access, or concern about retaliation. Use interviews and work-area observation to understand the story. Do not compare employees or shifts by raw idea counts or tie pay to suggestion volume.
Review the process monthly with employee representatives. Look at items that received no response, repeat concerns, and ideas delayed by authority or resources. Ask whether the intake form is too long, whether the right functions attend triage, and whether a person who raises an issue can see its status. The manager responsible for the system should remove barriers and publish changes to the response route.
Give the system a clear owner
Assign one coordinator to monitor the queue, but keep technical ownership with the function that controls the process. The coordinator may route an idea and prompt an overdue update; they should not approve an engineering change or quality disposition without authority. Each area should have a named owner and a backup for absences and shift coverage.
Protect time for triage and small tests. If employees can submit ideas only when production is idle, the system will miss the moments when work is hardest. Managers can reserve a short weekly review and plan small experiments into the schedule. For urgent issues, existing controls take priority over the improvement calendar.
Use this launch checklist:
Name the system coordinator, area owners, backups, and escalation contacts.
Publish the intake route in every work area and on every shift.
Separate urgent safety and quality reporting from routine ideas.
Set acknowledgement and decision targets that match local capacity.
Use a common record for owner, status, next date, and employee feedback.
Require safe test plans and relevant approvals before process changes.
Review response delays and repeated issues each month with employees.
Revise the system when the route itself creates waiting or discourages reports.
The first measure to collect is elapsed time from an idea’s receipt to its first acknowledgement, grouped by submission type. Pair it with a review of a few actual items so that a fast acknowledgement is not mistaken for a useful response. A culture of improvement depends on the quality of the follow-through.