Lean Leadership Routines for Manufacturing Supervisors
A Lean culture becomes visible in how leaders respond when the work misses its expected condition. A supervisor should go see the process, ask what condition changed, help the team test a cause, and follow up on the action. This guide gives you a one-week routine and observation log for a manufacturing cell.
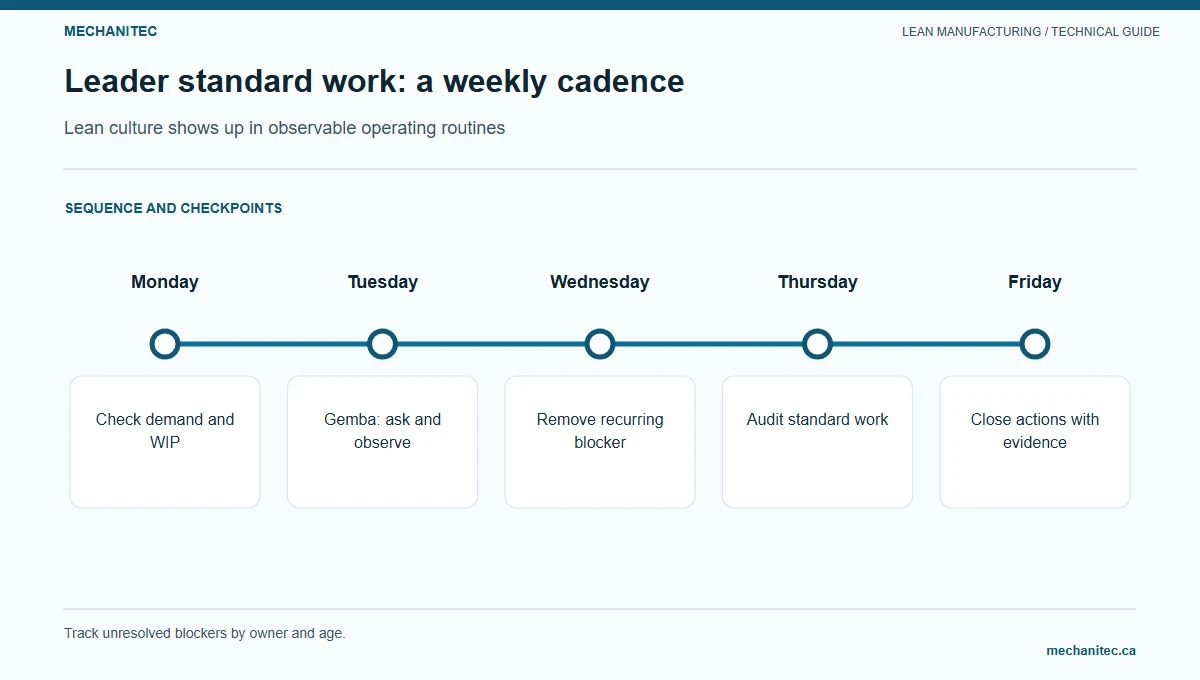
Schedule leadership work around the process
Use short, predictable checks to learn about safety, quality, delivery, and barriers. A huddle does not replace time at the work area, and a board does not replace a conversation with the person doing the work. The supervisor owns escalation and removes barriers; the operator explains the work and helps test a practical improvement; technical owners approve changes in their areas.
| When | Leader action | Question or evidence | Output |
|---|---|---|---|
| Each shift, start | Join a brief cell huddle | What is unsafe, abnormal, blocked, or not ready? | Owner and next response time for each barrier |
| Monday | Walk the product route with an operator | Where does work wait? Does actual work match the current standard? | One verified issue to investigate |
| Tuesday | Observe a setup or handoff | Which steps require machine stop, approval, or missing information? | Timestamped observation; no premature solution |
| Wednesday | Coach one problem-solving check | What fact supports the cause? What small test is safe? | Test, owner, measure, guardrail, and review date |
| Thursday | Follow up on open actions | Was the action completed and did the condition change? | Close, revise, or escalate with evidence |
| Friday | Review trend and standard | What did the team learn? Does the approved method need revision? | Documented next step and recognition of team contribution |
The calendar is a sample cadence, not an externally mandated schedule. Adjust it to shift patterns and risk. Immediate safety or quality issues go through the site’s formal escalation process without waiting for the next scheduled review.
Keep a short observation and follow-up log
| Date/shift | Observed condition | Operator’s view | Leader action | Follow-up |
|---|---|---|---|---|
| Monday, day shift (example) | Job waits for an approved drawing revision | Traveler and posted packet do not match | Hold job and contact document owner | Verify released packet before restart; review at next huddle |
| Tuesday, night shift (example) | Setup cart is missing a verified tool | Current storage location is shared by two cells | Ask team to map the retrieval path | Test a labeled location after safety and calibration review |
These log entries are illustrative. Do not write customer-sensitive details or personal performance notes on a public board. Keep controlled records in the site’s approved system.
Use questions that build problem-solving skill
- What did you expect to happen?
- What happened, and where can we verify it?
- What condition changed from the approved method?
- What is the smallest safe test that would distinguish possible causes?
- What must stay within safety, quality, and delivery requirements?
- When will we check the result together?
Do not treat a missed target as proof that someone failed. Avoid issuing a solution before seeing the work or praising a score without checking the conditions behind it. A supervisor may need to make a direct safety decision, but routine improvement should involve the people who perform the process.
Check governance quality
| Useful condition | Warning sign | Correction |
|---|---|---|
| Actions have an owner and due date | Same issue appears at every huddle with no decision | Escalate to the person with authority and set a response date |
| Measures have clear definitions | Shifts argue about what counts | Define scope, units, source, and sample window |
| Operators can raise problems safely | Signals stop after negative responses | Respond respectfully, investigate, and report what changed |
| Standards reflect approved work | Informal notes conflict with controlled instructions | Route changes through the document owner and train affected roles |
For the daily follow-up system after a Kaizen event, see the sustainment routine. For a specific event plan, use the machining-cell Kaizen guide.
Start with leader behavior people can observe
A lean culture is visible in how leaders respond when work does not follow the expected process. For a shop manager, the immediate decision is whether to listen, help contain the issue, and return a clear answer—or to ask for a higher output number without removing the barrier. Begin with a defined area and a small set of observable measures: operator ideas awaiting a first response, time from escalation to acknowledgement, missed tier-one huddles, leader observation time at the process, and countermeasures verified by their due date. These measures show whether the management routine works; they do not prove a broad change in “culture” by themselves.
Write the collection rules before tracking. An idea is awaiting response only after it enters the agreed log. Response time starts when the idea is recorded and ends when the owner communicates a decision or next step. A huddle counts as held when the named team meets and records its decisions; a calendar invitation is not evidence that it happened. A countermeasure is verified only when the process owner checks the result at the work and records what evidence supports closure.
Use a ten-minute tier-one huddle to surface barriers
Hold the huddle at the work area at a predictable time with the operator or team representative, team lead, and supervisor as needed. Keep the board focused on safety or quality abnormalities, schedule or flow status, staffing or material constraints, prior actions, and one request for help. Each item should name a condition, owner, due date, and escalation path. Do not read every metric aloud or turn the meeting into a public performance ranking.
When an operator raises a problem, the leader asks what was expected, what happened, and what evidence is available. The next question is what support or decision is needed now. If the team can safely test a reversible local change, define the test and stop condition. If the issue affects product acceptance, controlled instructions, machine safety, or another department, use the authorized escalation route. A huddle creates a fast path to a decision; it does not give the group authority to bypass controls.
| Minute | Prompt | Record |
|---|---|---|
| 0–2 | Is there an immediate safety, quality, or customer risk? | Containment, role notified, and any work or product status. |
| 2–4 | What is the current flow condition versus the agreed plan? | Count or queue measure with units and time window. |
| 4–7 | Which barrier needs a decision or cross-functional help? | Condition, evidence, owner, and required response. |
| 7–9 | Which prior action is due or recurring? | Verification, revised test, or escalation with reason. |
| 9–10 | Who will update the team and when? | Named person and next check time. |
Walk the process and coach problem solving
Schedule leader observation where the work occurs and vary the time so that different shifts and product conditions are visible. Ask the operator to show the standard, point to the abnormality, and explain what happens next. Listen before prescribing a countermeasure. If the standard is difficult to follow, ask which condition makes it difficult and observe the step; do not assume that the worker needs another reminder.
Use questions that build a repeatable problem-solving habit: What should happen next? What happened instead? When and where did the gap first appear? What did you check? What would make a small test safe and informative? Who must approve it? When will we review the evidence? The leader can offer technical knowledge, but should make the next decision and owner explicit. Coaching is not withholding help; it is helping the team understand the condition and choose a controlled response.
Work one recurring materials issue through the system
The following example is fictional. On day 1, an assembly cell reports that a purchased bracket is missing from several kits. The team records the part and revision, job numbers, kits affected, quantity missing, and the next production need. The lead checks nearby approved locations and the inventory record without moving unidentified or held material into production. If the shortage threatens a customer order, the scheduler and purchasing owner are contacted through the site’s priority route. The huddle records containment, current schedule impact, and when the team will update the cell.
On day 7, the materials owner returns with the transaction history and receipt record. The team finds that a replenishment signal was entered but the received quantity was posted to a different location. The group does not label this a worker failure. It verifies the physical stock and system state under the approved inventory process, then tests a clearer location confirmation on the next replenishment. The owner and end date are written on the action register. If the evidence instead points to supplier delivery or a drawing change, the team routes that issue to the appropriate owner rather than forcing the same explanation.
On day 30, the leader checks whether the same shortage or transaction mismatch recurred, whether the signal and location records agree, and whether the affected shifts can explain the updated method. If the test helped, the owner submits the change for controlled approval and updates training and standard work. If the issue returned, the team reopens the problem with the new evidence. The example describes a management response pattern; it does not claim that a specific company achieved a measured result.
| Date / stage | Evidence | Owner and next step | Closure test |
|---|---|---|---|
| Day 1: report and contain | Part, revision, job, quantity missing, need time, inventory state | Lead confirms approved stock and routes schedule risk. | Cell receives a clear status and next update time. |
| Day 7: investigate | Receipt, transaction, location, and physical count checked | Materials owner tests location confirmation on next replenishment. | System and physical quantity reconcile for the sample. |
| Day 30: verify or reopen | Recurrence, transaction accuracy, and shift feedback | Process owner submits an approved standard change or reopens the issue. | Evidence covers the defined sample and affected shifts. |
Use measures to find management-system gaps
Track unresolved ideas by age and first-response time, not just the number submitted. Review missed huddles by shift and reason. For leader observation, record whether the planned time occurred and what process condition was learned, not the number of visits alone. For countermeasure closure, compare due actions with those verified on time and separately track reopened or recurring items. Keep raw counts and the denominator beside percentages so a small sample is visible.
These are process signals, not employee rankings. A rise in ideas may mean more problems are being surfaced; a decline may reflect fewer problems or reduced trust. Ask workers what the log misses and whether leaders return decisions promptly. A short pulse conversation and observed huddle quality can add context, but do not turn a few comments into a claim that the whole organization changed.
Check governance and overlap before expanding
Leaders should distinguish an operational standard from a personal preference. Any change to inspection, work sequence, safety control, or controlled document must have the required technical approval. A leader who asks for a trial also owns the route for approval, resourcing, and communication across shifts. The team should not be held accountable for a decision outside its authority.
This article focuses on visible leadership behavior and feedback response. A separate leader-standard-work guide can explain the supervisor’s cadence in more detail; a momentum article can explain how to sustain review and escalation. Link to those pages only where they add a distinct next step. Keep the example and measures here centered on whether workers can raise a barrier and receive a useful, traceable response.
Source
- Lean Enterprise Institute: Standardized work — explains the elements of a defined work method and its role in ongoing improvement.