Home » Successful Implementation of Kanban in Manufacturing
Successful Implementation of Kanban in Manufacturing
Contents
A Kanban card is a production or withdrawal signal. It authorizes a defined quantity to move or be replenished after downstream use; it is not a general instruction to keep every machine busy. This guide shows how to bound a replenishment loop, calculate a starting card count, and handle shortages, lost cards, and quality holds.
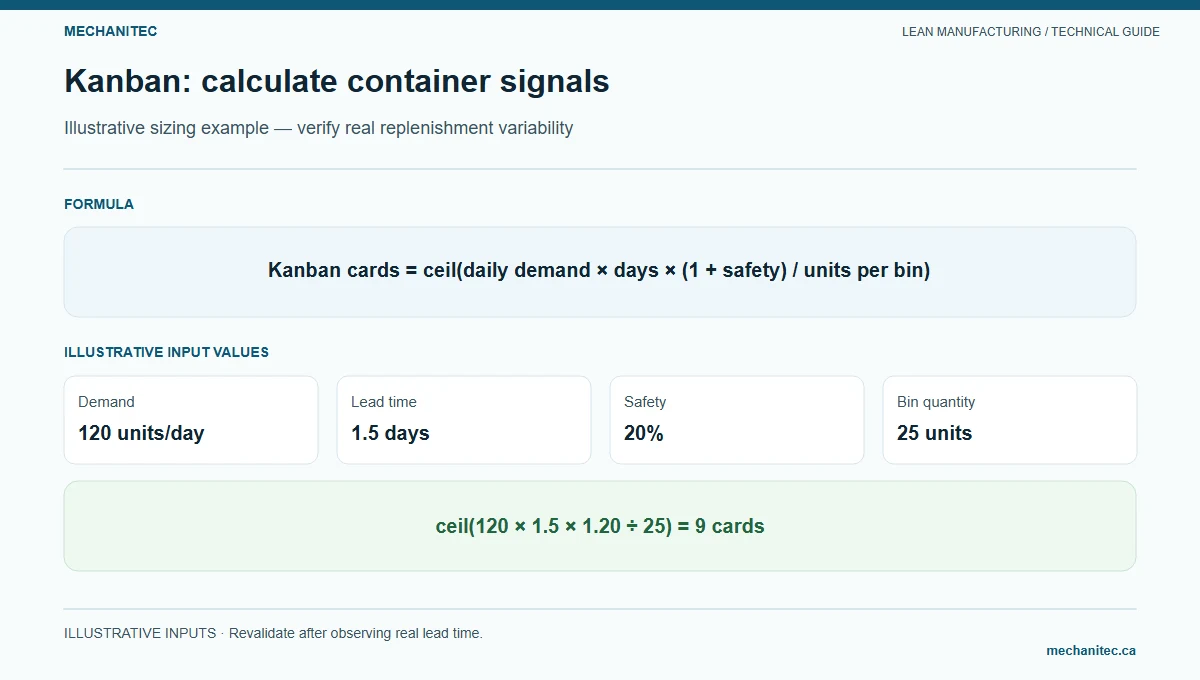
Illustrative sizing example — verify real replenishment variability. Mechanitec instructional diagram.
The calculation is an illustrative example, not a result from the anonymous “case study” previously described in this article. The inputs must come from the actual part family and replenishment route. Kanban levels are starting controls that need review when demand or replenishment conditions change.
Define the loop before counting cards
Name the customer process that consumes the part and the supplying process that replenishes it. Set a specific supermarket location and a maximum container quantity. The loop begins when a container is consumed or withdrawn and its signal returns; it ends when the replenished container is accepted and available at the agreed location. Include signal collection, queueing, changeover, production, inspection if required, movement, and put-away in the replenishment time.
Example two-bin replenishment loop
Step
Action
Control
1
Using process takes the next identified container.
Use the part number and location shown on the card; do not substitute a similar part.
2
Empty container and card move to the collection point.
The signal is visible and collected at the agreed interval.
3
Supplying process produces or picks the authorized quantity.
Do not produce ahead of valid signals except under an approved exception.
4
Part is checked as required and returned to the supermarket.
Return it to the marked location and restore the card to the container.
5
Using process withdraws the full container.
Repeat the loop; review exceptions and actual lead time.
A physical card can include the part number and description, supplying and consuming process, container quantity, storage address, card identifier, and any approved traceability or handling information. A barcode or electronic signal can carry the same information. Use a controlled card master so a part, location, or quantity change does not create conflicting instructions.
Illustrative Kanban card fields
Field
Sample value
Why it is present
Part number / description
F-217 / M8 machine screw, approved finish and revision
Identifies exactly what the signal authorizes.
Supplying process
Fastener supermarket / replenishment route B
Shows where replenishment starts.
Using process / location
Assembly station A / rack R-02
Shows the authorized destination.
Container quantity
25 pieces
Bounds the quantity moved or produced per signal.
Card number
3 of 9
Helps reconcile the approved number of cards in the loop.
Revision / handling
Controlled card master reference
Routes specification, quality, or handling changes through the authorized process.
Walk the two-bin event from assembly to replenishment
Imagine assembly station A empties its first 25-piece bin of F-217 machine screws while the second bin remains available. The operator removes the card from the empty bin and places it in the marked collection slot. The card identifies the exact part, revision, finish, supplying supermarket, destination rack, and container quantity. The operator does not order a substitute screw or borrow from an unverified bin.
At the agreed milk-run time, the material handler collects the card and scans or records it at the route point. The card moves to the supplying process, where the authorized team sees one demand signal for 25 pieces. The supplying process checks the part identity and current approved revision, picks or produces the quantity, records any required lot or supplier trace, and returns the filled container with its card. The handler scans the return and moves the bin to rack R-02. Assembly checks the label, quantity, and status before use. The empty bin then returns through the standard loop.
Two-bin Kanban handoff for the F-217 fastener
Event
Who acts
Signal or quantity
Required control
First bin empties
Assembly operator
One card; 25 pieces consumed
Use the second identified bin; do not create an informal order
Signal is collected
Material handler
Card scan and timestamp
Route it to the named supplier point on the next scheduled loop
Replenishment is authorized
Supplying process
One card permits one 25-piece container
Do not make an extra bin because equipment is available
Container is returned
Material handler
One full accepted bin and its card
Verify location, label, quantity, and any required traceability
Bin is received
Assembly operator
Two-bin loop resumes
Reject or quarantine a mismatched or held container
Production Kanban and withdrawal Kanban perform different jobs. A production card authorizes the supplying process to make a defined amount. A withdrawal card authorizes movement of a defined amount between locations. A single loop can use one signal type or both, depending on whether the material handler moves stock from a supermarket or the supplier replenishes the point of use directly. The card and standard work must make that distinction clear so no team produces twice for one withdrawal.
Use “no make without a valid production signal” and “no move without a valid withdrawal signal” as operating rules where the system design supports them. State approved exceptions, such as a controlled trial or a documented emergency response, in the local procedure. A card lost in transit is not permission to create another. The loop owner reconciles circulating cards, containers, open work, and transactions before authorizing a replacement.
Verify the inputs behind the card count
Measure demand for the exact part and time period used in the formula. If 120 pieces per day is an average across several revisions, projects, or shutdown weeks, confirm that it represents the replenishment period being designed. Record both typical usage and meaningful spikes. Use a consistent unit: pieces per working day must pair with replenishment lead time in working days. Do not multiply by calendar days unless demand and replenishment have been converted to that calendar.
Measure lead time from signal availability to accepted stock at the agreed receiving location. Include card collection, waiting for a production slot, setup, run time, inspection, transport, and put-away. If inspection holds or supplier paperwork often delay availability, include that observed time. The term “one day lead time” is incomplete without its start, end, calendar, and item scope.
Check min/max, supplier minimum orders, lot restrictions, shelf life, storage capacity, and quarantine rules. The formula gives an initial number of containers; it does not override these constraints. A perishable item may need a lower maximum, while an imported fastener may need a separately authorized disruption plan. Keep a defined buffer visible instead of hiding it in extra cards.
Calculate an initial card count
For a fixed container size, use this common starting calculation:
Cards = round up [daily demand × replenishment lead time × (1 + safety factor) ÷ container quantity]
Use the same time unit for demand and lead time. “Replenishment lead time” means the full measured loop from signal until accepted stock is available again, not only machine run time. The 20% policy value below is illustrative; choose an allowance only after reviewing measured demand or supply variation and the site’s approved material-control rules. It does not guarantee a service level.
Illustrative card-count calculation; all inputs are hypothetical
Input
Value
Unit or assumption
Average daily demand (D)
120
pieces per day for one stable part number
Replenishment lead time (L)
1.5
days from signal to accepted stock at the point of use
Safety factor (S)
0.20
20% illustrative policy allowance, not a universal service-level guarantee
Container quantity (C)
25
pieces per container
Calculation
120 pieces/day × 1.5 days × (1 + 0.20) ÷ 25 pieces/card = 8.64 cards; round up to 9 cards.
Maximum loop quantity at full containers
9 cards × 25 pieces/card = 225 pieces, or 1.875 days of the assumed demand.
Validate the result against observed shortages, actual supplier and process variation, container handling, lot-size restrictions, inspection requirements, and the customer service target. Review the number after a meaningful demand or lead-time change. If you use a one-card/two-bin design, solve for bin quantity instead; do not confuse two bins with two cards. In this example, 9 full cards represent 225 pieces. That is 25 pieces more than the 180 pieces of average demand during 1.5 days and 45 pieces above that gross lead-time amount. The extra amount follows from the chosen 20% policy allowance and rounding to whole containers; it is not a physical law or a promise that shortages cannot occur.
Interpret the illustrative 9-card result
Calculation step
Result
Meaning
Average demand during lead time
120 × 1.5 = 180 pieces
Gross demand represented by the stated average inputs
Illustrative policy allowance
180 × 0.20 = 36 pieces
Chosen planning allowance; not observed demand or guaranteed protection
Quantity before container rounding
180 + 36 = 216 pieces
Gross demand plus the illustrative allowance
Containers required
216 ÷ 25 = 8.64; round up to 9
Whole-card requirement for 25 pieces per container
Full loop quantity
9 × 25 = 225 pieces
Maximum quantity if all cards represent full containers
The team sets a maximum of nine circulating cards in this example. A card may be at the using station, on the milk run, in the supplying queue, or attached to a full container; its location should be visible. The loop owner checks that a card is not counted as both an open signal and a full container. The minimum available quantity and reorder trigger depend on where the signal is released, how frequently it is collected, and whether one or two bins are used.
Do not let a planner or machine operator make extra material simply because the supermarket looks low. If the trigger is reached, use the valid signal. If the trigger has not been reached but a documented customer or disruption risk requires an exception, record the authorized quantity, reason, scope, and expiry date. This preserves the signal as a meaningful control while giving the team a traceable route for unusual conditions.
Make each exception visible
Exception response for a controlled replenishment loop
Condition
Immediate response
Record and recovery
Empty bin with valid signal
Move the card to the collection point and use the next authorized container.
Record a shortage if replenishment is not available within the agreed loop time.
Lost card
Check other circulating cards, on-hand containers, open production, and transactions before making a replacement.
Have the loop owner authorize and log a replacement to prevent duplicate replenishment.
Supplier or internal delay
Notify the material planner and affected process as soon as the expected return is at risk.
Use the approved shortage/expedite process; record cause and actual lead time for recalculation.
Quality quarantine
Identify and segregate the suspect lot under the site’s nonconforming-material process.
Do not return held parts to usable stock. Quality disposition controls release; replenish only through an authorized signal or documented exception.
Demand spike or schedule change
Confirm the change and its duration with planning before releasing additional material.
Record the temporary control and expiry/review date; update the standard only after the loop is remeasured.
When a Kanban loop is a poor fit
Do not use a fixed loop for sporadic, engineered-to-order parts without a stable repeated demand pattern; plan those jobs against their actual orders.
Do not hide an unreliable process by adding cards indefinitely. First identify whether delay comes from signal collection, queues, setup, downtime, quality, supplier variation, or transport.
Keep safety stock and buffers visible. Removing cards before the replenishment process is stable can create shortages; retaining excess cards can hide a constraint.
For supplier loops, agree on the signal, quantity, delivery window, packaging, quality records, ownership, and escalation with the supplier before the signal becomes a purchase or production authorization.
Run a short validation and exception review
For the first week, count cards and containers at the start and end of each shift. Compare the number of valid signals with production starts and completed containers. Record actual signal-to-return time, shortage duration, and material that is awaiting inspection or disposition. Check that each card has one matching container and each replenishment has one authorized signal.
Seven-day Kanban loop validation log
Day / shift
Cards issued / returned
Actual loop time
Exception
Owner and due time
Resolution evidence
Date and shift
Count by controlled card ID
Signal timestamp to accepted stock at location
Lost, duplicate, late, held, damaged, or wrong quantity
Named role and response deadline
Reconciled card, approved disposition, or corrected transaction
Investigate when a card is missing, two containers appear for one signal, an empty bin has no card, a returned container is short, or a held lot is mixed with usable material. Keep suspect inventory separate and follow the site’s quality process. Record a root cause only after the team checks the transaction, physical movement, and timing. Do not adjust the card total simply to make a shortage disappear from the log.
Review the loop after one week and again after demand or lead time changes. If demand is temporary, use an approved temporary control with an owner and expiry date. If supplier or process variation is higher than the allowance, stabilize the loop or adjust the authorized quantity with evidence. If stock grows older or becomes obsolete, check whether cards are being returned after actual use and whether the forecast or part mix changed.
Kanban setup checklist
Select one repeated item and name its using and supplying processes.
Measure demand and the full signal-to-accepted-stock lead time in matching units.
Set one approved container quantity and identify lot, inspection, and quarantine rules.
Calculate a starting loop size; document any safety policy and check min/max constraints.
Label the supermarket slots, card IDs, route, pickup frequency, and responsible roles.
Train the team on no-make/no-move rules, lost-card reconciliation, and quality holds.
Log the first week’s card count, shortages, actual lead time, and exceptions before adjusting the loop.
Assign one named loop owner to maintain the card master, audit the supermarket quantity, and coordinate changes with the using and supplying processes. The first review should compare expected and actual signal-to-return time for each card, not just the end-of-week inventory total.
Sources
Lean Enterprise Institute: Kanban — describes Kanban as a signal that authorizes production or withdrawal and notes the need for timely, reliable signal return.