Home » Just-in-Time Production for Mixed-Volume Manufacturing
Just-in-Time Production for Mixed-Volume Manufacturing
Contents
Just-in-time (JIT) production aims to make and deliver what is needed, when it is needed, in the amount needed. For a mixed-volume shop, use it as a controlled material and information flow design—not as a blanket instruction to remove inventory. Begin with a stable product family and a reliable replenishment loop, then measure whether service and quality hold as WIP changes.
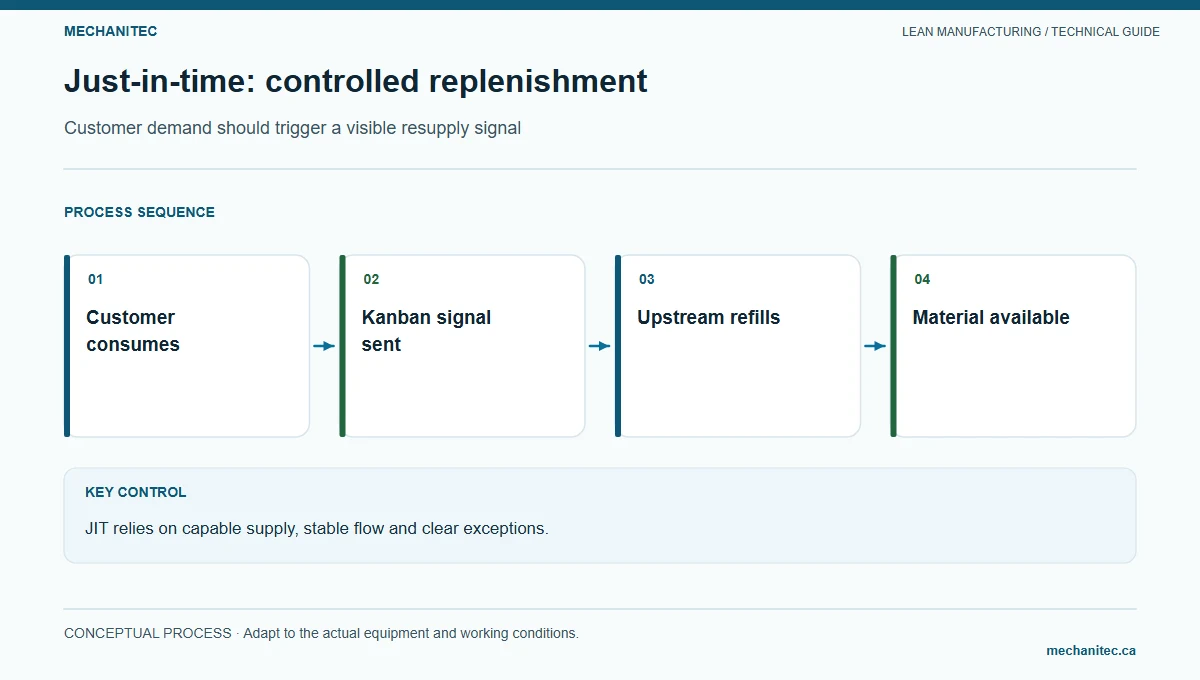
Customer demand should trigger a visible resupply signal. Mechanitec instructional diagram.
The bracket example below is fictional. Its values demonstrate the method and are not a real company case or a recommended stock level.
Check the preconditions before reducing inventory
Demand and product mix are visible enough to set a replenishment rule.
The supplying process can make acceptable parts consistently, with a defined defect and escalation path.
Material, supplier lead time, receiving, and transport are recorded with units and dates.
Container quantity, storage location, ownership, and replenishment signal are clear.
There is a contingency for supplier disruption, equipment failure, quality holds, and demand changes.
If a process produces defects, has unstable lead time, or relies on unavailable supplier data, reducing the buffer can expose the instability without fixing it. Resolve critical quality or safety risks first. For high-mix or intermittent items, make-to-order planning or a hybrid policy may fit better than frequent replenishment for every SKU.
Establish a baseline for demand, supply, and stockouts
Collect enough history to see product mix and replenishment variation before changing the buffer. Use one item or a small family that shares a route and replenishment rule. Record daily demand, scheduled time, actual production availability, order quantity, delivery dates, received quantity, inspection status, and point-of-use withdrawals. State whether lead time uses working or calendar days.
For each supplier order, record release and the date accepted material becomes available. Review the range, late deliveries, minimum order quantities, and partial shipments. Separate normal demand from one-time orders. Record stockouts, line stops, expedites, and quality holds with dates and affected jobs. This evidence helps distinguish supplier delay from internal release, receiving, and status problems.
Baseline record for a JIT material loop
Input
Definition and unit
Source / owner
Review question
Daily demand
Pieces required per working day, by SKU or family
Customer schedule or approved production plan
Is the mix stable enough for a repeating signal?
Supplier lead time
Order release to accepted quantity at point of use; calendar or working days stated
Purchase order, receipt, and inspection timestamps
What are typical and late delivery conditions?
Supply constraints
Minimum order, pack quantity, delivery frequency, and transport route
Supplier agreement and receiving records
Can the supplier support the proposed cadence?
Internal availability
Usable stock, pipeline quantity, holds, and location
Physical count reconciled to inventory system
Are held or obsolete pieces counted as usable?
Failure history
Stockout count, duration, expedite, line stop, and cause
Production and purchasing records
Which exception threatens service most?
Reconcile physical stock with the inventory record. Count available, in-transit, inspected, quarantined, and obsolete quantities separately. A quality hold is not a production buffer, and an unshipped purchase order is not material at the point of use. Use the same item identifier, revision, unit, and pack size in the plan, label, and transaction.
Set operating conditions before opening a pull loop
Identify the pacemaker process that controls sequence and pace for the selected family. Do not release independent schedules at every downstream step and expect a pull signal to correct conflicting priorities. Confirm the transport route, pickup frequency, container standard, and signal owner. The route must work across shifts, breaks, and temporary staffing changes.
Level the schedule when the mix and process allow it. A repeating sequence can reduce peaks that overwhelm a supplier or shared machine, but it does not remove variant, setup, or capacity constraints. Set pitch—the repeating production and transfer increment—only after checking demand and container quantity. If the route changes, recalculate pitch and verify each operation’s capacity.
Define the receiving status. When inspection or document review is required, replenishment lead time ends when accepted material is released for use, not when the truck arrives. Keep pending, rejected, and revision-uncertain stock separate from production-ready containers.
Write standard work for withdrawal, signal collection, authorized quantity, receiving checks, and handoff ownership. A signal authorizes one defined replenishment. It is not a forecast or permission to make extra stock. Define how the team recovers a lost card or unreadable barcode without creating duplicate production.
Compare demand pace with actual process conditions
Suppose a fictional customer needs 60 accepted enclosures across a five-day work week. Average demand is 60 ÷ 5 = 12 units per working day. If the operation has 450 planned production minutes per day, takt is 450 ÷ 12 = 37.5 minutes per unit. Takt describes the demand pace; it does not establish that every process can meet that pace or that demand is uniform across product variants.
For mixed-volume production, segment part families that share a route and setup pattern. Record demand variability and changeover time. A large batch may reduce setup frequency but increase queue time and delay the next variant. A small batch may improve flow but can overload a process with long setups or unstable availability. Test the trade-off using actual customer mix and approved capacity.
Stage one supermarket replenishment pilot
A supermarket is a controlled buffer where a downstream user withdraws a defined quantity and the supplying process replenishes what was used. Choose one repeat item with a stable route and clear container. Assign a unique item and location, label the standard quantity, define the withdrawal signal, set an owner, and specify what happens when replenishment is late or quality is in doubt.
Illustrative mixed-volume replenishment loop
Step
Role
Control and record
1. Withdraw
Downstream operator
Take one identified container; remove or scan its replenishment signal
2. Return signal
Material handler or planner
Route the signal to the named supplying process; timestamp receipt
3. Replenish
Supplying cell
Make only the authorized item and quantity; record completion and any quality hold
4. Verify
Receiving operator
Check item, quantity, revision, and status before use
5. Escalate
Planner and process owner
Log shortages, late replenishment, changed demand, or supplier exceptions
Do not replenish a container from memory when its signal is missing. Reconcile the loop, investigate the cause, and protect traceability. A pull signal does not authorize use of unapproved material or release of a quality hold.
Calculate a starting card count with explicit assumptions
For a fixed-demand example, one common starting relationship is:
Containers = round up[(daily demand × replenishment lead time × (1 + safety factor)) ÷ container quantity].
Assume, only for illustration, 12 pieces per working day, a 1.5-working-day replenishment lead time, a 10% safety factor, and 5 pieces per container: 12 × 1.5 × 1.10 ÷ 5 = 3.96, rounded up to 4 containers. This starting count assumes those inputs describe the same item and time units. It does not guarantee a service level; measure actual shortages and excess, then adjust under an approved material-control method.
Replenishment measures for a mixed-volume pilot
Measure
Definition
Review
Replenishment lead time
Signal release to accepted material available at point of use
Distribution by item and supplier, not only average
Shortage event
Demanded material unavailable when required
Count, duration, cause, and affected orders
Inventory in loop
On-hand pieces in the defined supermarket and replenishment pipeline
Quantity and age, segmented by item
Service
Orders or operations supplied when required, with one stated denominator
Trend with demand mix and exceptions
Quality hold
Material not authorized for production pending disposition
Keep separate from available stock and never count as usable buffer
Worked example: demand of 100 pieces per day
Illustrative example — not observed plant performance. A mixed-volume assembly family consumes 100 accepted fittings per working day. The measured replenishment lead time from order release through receiving and inspection to point of use is two working days. The supplier ships in packs of 25. Gross demand during the measured replenishment lead time is 100 × 2 = 200 pieces, or 200 ÷ 25 = 8 packs. This is the minimum quantity exposed by the stated average inputs before a protective policy is considered.
For a pilot, the team might hold one additional pack as a separately identified protection quantity while it measures real variation. The initial total would then be 9 packs, or 225 pieces. That extra pack is a temporary assumption, not a universal safety factor. The owner records why it exists, what event it protects against, and the date to review it. If the extra pack is not enough to cover the observed high-end delay, the team changes the supplier agreement, lead time, pack rule, or authorized buffer based on evidence.
Use a withdrawal card or electronic signal for each 25-piece pack. The signal identifies the fitting, revision, quantity, source location, and receiving point. The supplier cell or planner records when it is received. Replenishment is complete only when the correct pack passes required incoming checks and becomes available at point of use.
A two-bin arrangement can make the signal simple: use one labeled bin and send its signal when it is empty; draw from the second while the first is replenished. It does not automatically reduce inventory. If each bin contains only one day of demand while replenishment takes two days, the second bin may run out first. Size the bins to measured replenishment exposure and any approved protection quantity. Calculate total pieces and verify timing before the pilot.
If an order minimum forces a larger batch than the calculated requirement, document the commercial constraint and evaluate a different cadence, supplier agreement, shared delivery, or hybrid policy. If demand falls sharply, stop signals from creating obsolete stock and revise the authorized plan through the owner.
Use a seven-day exception log
Capture every late, missing, damaged, held, or duplicate signal during the pilot. This helps the team see whether the loop fails because of supplier delivery, internal transport, receiving inspection, inventory accuracy, or demand changes. Record facts first. “Supplier issue” is too broad to guide corrective action unless the team identifies the event.
Seven-day JIT exception log
Day / time
Item and signal
Observed exception
Immediate control
Owner and due time
Closure evidence
Timestamp
SKU, revision, container quantity
Late, lost, duplicate, short, damaged, or held
Protect affected order; separate suspect stock
Name a role and response time
Receipt, count, approved disposition, or corrected transaction
At the daily review, compare signals with containers withdrawn and replenished. Check the oldest open signal, oldest available stock, and any item near its expiry or engineering-change date. Do not close an exception because a truck arrived; verify that the right item and quantity were accepted and the record reconciles. Escalate safety or quality conditions through the site’s established procedure.
Check supplier readiness and run a bounded pilot
Before changing order frequency, review the proposed cadence with the supplier and internal receiving team. A card count that works on paper can fail if pickup times, pack sizes, labels, or inspection documents do not match the supplier’s process. Keep the agreement in the normal purchasing channel and name the person who can approve a change. Do not treat a pilot signal as a contractual order without the required authorization.
Supplier readiness checks before a JIT pilot
Check
Evidence to confirm
If it is not ready
Item identity
Part number, revision, approved source, and pack label match
Resolve the mismatch before issuing a replenishment signal
Order cadence
Supplier confirms release, pickup, delivery, and minimum quantity
Keep the current policy or agree on a different cadence first
Quality status
Required certificates, inspection, traceability, and hold process are clear
Do not count pending or suspect stock as available
Exception contact
Named buyer, supplier contact, and escalation response time
Define the response route before reducing the buffer
Recovery plan
Approved response for disruption, late shipment, or quality rejection
Keep a deliberate protection quantity or defer the pilot
A bounded 30-day pilot can begin with a single item, one receiving point, and an identified replenishment owner. In week one, verify labels, locations, timestamps, and signal movement without reducing the current authorized stock. In week two, run the proposed container and cadence while logging every exception. In week three, check shortages, excess, response times, and inventory accuracy with the operators and supplier contact. In week four, compare the same measures to baseline and decide whether to adopt, revise, or stop.
Set decision criteria before the pilot. For example, require every signal to be traceable, no unresolved quality hold to enter available stock, and all shortage events to have an owner and documented response. The team can set additional service and stock targets from its customer commitments. If a safety or quality issue occurs, follow the applicable containment process immediately; do not wait for a weekly review.
Review disruptions and applicability limits
Review the pilot weekly with the supplying cell, planner, material handler, quality, and purchasing where suppliers are involved. Test a changed demand week, late delivery, rejected batch, and replenishment signal failure. Define who can raise or lower the authorized buffer and how the change is recorded.
JIT is not “zero inventory.” A buffer may be necessary while the team improves process reliability or manages supplier risk. If demand or lead-time variation overwhelms the loop, pause further inventory reductions, identify the dominant causes, and revise the design. Check long minimum-order quantities, transport disruption, single-source supply, engineering changes, seasonal demand, and shared supplier capacity. JIT can move inventory exposure upstream without removing the risk. The buyer, planner, and process owner should define who approves a deliberate exception stock level. For card setup and exception controls, see the manufacturing Kanban guide. For a whole-route material and information map, see the VSM tutorial.
JIT pilot checklist
Select a repeat item with a clear route, owner, revision, and consumption signal.
Verify demand, pack size, lead time, supplier minimum, delivery calendar, and incoming inspection.
Reconcile physical stock and the system record; separate holds and obsolete inventory.
Define the pacemaker, transport route, signal handoff, replenishment quantity, and lost-signal response.
Calculate gross lead-time demand and document any temporary protective quantity.
Run the exception log without relaxing approved quality controls.
Review shortages, excess, stock age, supplier variation, and service before changing the authorized buffer.