Home » Apply the Five Lean Principles to a Fabricated Enclosure Order
Apply the Five Lean Principles to a Fabricated Enclosure Order
Contents
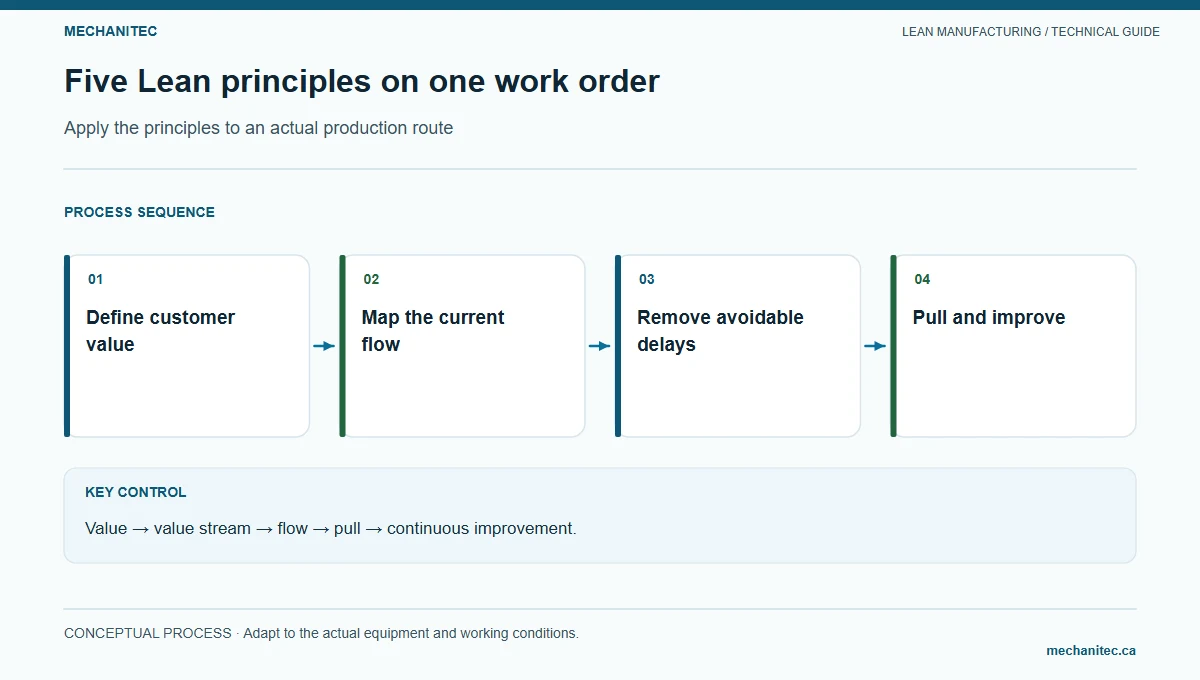
The five Lean principles become useful when you apply them to one customer order from specification through delivery. This walkthrough follows a fictional fabricated enclosure. It shows how value, the value stream, flow, pull, and continued improvement shape the same job; the example is not a real company case or performance claim.
Apply the principles to an actual production route. Mechanitec instructional diagram.
Start with the customer’s required result
For the example order, the customer needs an enclosure built to the approved drawing revision, with specified material, coating, documentation, quantity, and delivery date. The sales or engineering team confirms the acceptance conditions before release. Do not treat internal preferences, unused features, or a convenient batch size as customer value without checking the requirement.
Trace the whole value stream
Follow the order through design release, material procurement, cutting, forming, welding, outside coating, final inspection, and shipment. Map both physical parts and information: the drawing revision, bill of material, purchase order, traveler, inspection plan, and delivery instruction. Record queues, rework, batch transfers, and the reason for each handoff.
Revision and required characteristics move to planning
Is the released packet complete and accessible?
Material procurement
Correct grade, thickness, and quantity available
Purchase order, supplier promise, receipt and quality status
Is a long lead item delaying release?
Cut and form
Blanks and formed features meet the drawing
Traveler, first-piece check, quantity and next operation
Does a large batch create waiting or damage risk?
Weld
Assembly meets approved drawing and procedure
Current instructions, fixture, inspection and hold status
Does work wait for missing fit-up, fixture, or approval?
Coat and inspect
Finish and acceptance criteria are met
Outside-process dates, lot traceability, acceptance record
Is the supplier or inspection queue visible?
Ship
Correct order and documents arrive by commitment
Final accepted quantity and shipping authorization
Did upstream delays become last-minute expediting?
Improve flow without bypassing controls
Identify where a part can move in a tighter sequence and where a buffer or outside process prevents continuous flow. A physical rearrangement is not the first answer if information, material, setup, quality, or capacity is the real constraint. Verify safe handling, required inspection, process qualifications, and customer controls before changing the route.
Use pull only where a defined signal can work
At a repeat-use material point, a downstream withdrawal can trigger a replenishment quantity. For the one-off enclosure, the drawing-specific blank or custom coating specification may need order-based planning rather than a generic supermarket. The planner sets a control that reflects the part’s actual demand pattern and supplier lead time. No upstream operation should make a different revision just because a card or schedule is stale.
Make improvement a repeatable feedback cycle
After the order ships, review what was late, reworked, expedited, or unclear. Use a specific measure such as elapsed time from complete engineering release to accepted shipment, queue age before welding, or first-pass acceptance at inspection. The owner records the sample, definition, and next action. Test a small change, verify the result, and revise the approved method only when authorized.
Five principles applied to the same enclosure order
Principle
Question for this order
Responsible role
Evidence
Value
What specification, date, quantity, and documentation does the customer require?
Sales/engineering with customer requirements owner
Approved order and drawing revision
Value stream
Which physical and information steps take the job to shipment?
Planner and cross-functional team
Observed route with queue and handoff data
Flow
Where can accepted work move safely with less waiting?
Operators and process owners
Cycle, queue, batch, and quality records
Pull
Where does a reliable downstream signal fit this order or repeat item?
Planner and material owner
Defined trigger, quantity, and replenishment route
Perfection
What did this order teach the team, and what will be tested next?
Process owner with affected roles
Review record and approved follow-up action
Lean methods do not remove the need for engineering approval, quality disposition, safe work, or supplier coordination. If the order is highly engineered and has no repeat route, use order-specific planning and focus the improvement on a stable sub-process rather than forcing a one-piece flow model.
Keep the example’s product family and demand interval consistent. Suppose a fictional shop receives an order for 10 enclosures per production day, with 450 minutes available for the route each day under its stated calendar rule. Takt is 450 ÷ 10 = 45 minutes per enclosure. The observed touch or processing times for a representative enclosure are 12 minutes at laser cutting, 18 at forming, 40 at welding, and 12 at final inspection. These illustrative times do not include setup, shared-equipment availability, coating batch residence, inspection waits, rework, or material delays. Welding’s 40-minute time appears close to takt, so the team should verify capacity and product mix before assuming it can support demand.
The order’s customer value includes the approved drawing and revision, specified material and finish, acceptance evidence, quantity, and promised date. If one of those conditions is incomplete, planning should not release work as though the order were ready. The team confirms the exact requirement with the responsible customer or engineering role and records the approved interpretation before the job proceeds.
Illustrative current and proposed queue condition; caps are test assumptions, not achieved results
Location
Current WIP
Proposed pilot cap
Flow question and guardrail
Before welding
20 enclosures
10
Can the weld cell replenish against downstream acceptance while preserving fit-up and inspection?
Before coating
30 enclosures
10
Does the supplier require a batch or finish sequence that limits release frequency?
Before final inspection
10 enclosures
10
Is inspection capacity and documentation complete? Do not bypass release criteria.
Total at the three queues
60 units = 6 demand days at 10/day
30 units = 3 demand days if caps hold
Arithmetic comparison only; measure actual lead time, throughput, and late orders.
The proposed caps do not prove that the route will flow better. Before testing, the team checks whether welding, coating, or inspection can accept the next job, how an exception is signaled, and where work waits when a cap is full. If coating must run in a batch, define a controlled batch window and owner instead of pretending one-piece flow is practical. The shop records job age, material status, held quantity, and the reason each job waits.
Apply value, stream, flow, pull, and improvement in sequence
1. Define value with the customer requirement
Translate the order into measurable acceptance conditions: part identity and revision, material, dimensions or features, finish, documentation, quantity, and delivery. The team distinguishes those requirements from internal preferences. A feature cannot be removed because it appears non-value-adding; engineering and the customer requirement owner determine whether it is necessary.
2. Trace the value stream
Follow the information and the physical enclosure from order entry through engineering release, procurement, cutting, forming, welding, coating, inspection, and shipment. Record every queue, handoff, status, batch, and hold. The current-state map should show actual behavior, not an idealized routing list. Check whether supplier lead time, document approval, or missing material drives delay before changing a machine layout.
3. Improve flow where the process permits
Look for a safe sequence that lets accepted work move to the next operation without avoidable waiting. A smaller transfer batch may expose defects earlier and reduce queue time, but the shop must validate handling, setup frequency, finish constraints, and inspection requirements. Do not move a part past a hold, skip a required check, or create excessive setups in the name of flow.
4. Use pull where a reliable signal is possible
For a repeat-use purchased fastener or standard enclosure component, a downstream consumption signal may trigger replenishment if demand, lead time, quality status, pack quantity, and supplier response are reliable. The custom enclosure itself may remain order-planned because its drawing and finish are specific to the customer. Use a signal only where the trigger and next action are explicit. No upstream operation makes a superseded revision because an old schedule or card is still visible.
5. Learn from each completed order
After shipment, review which condition caused waiting, rework, expediting, or confusion. Keep the sample size, definition, and owner with the measure. Choose one test, verify it under representative work, and update the approved method only when authorized. “Perfection” in this sequence means continuing to learn and improve the value stream; it is not a claim that defects can be eliminated by a slogan.
Choose measures that connect the principles
Use a small set of measures that reflect the customer and the route: order lead time from complete release to accepted shipment, queue quantity and age before the identified constraint, first-pass acceptance at a defined step, schedule attainment, and material or revision exceptions. Report units, numerator and denominator, period, family, and sample. A shorter queue with more late orders is not a better flow result. A higher output count without demand may create unwanted inventory.
Five-principle review sheet for the illustrative enclosure order
Principle
Evidence to review
Owner’s question
Next action
Value
Approved order, drawing, finish, documentation, and due date.
Are acceptance conditions complete and understood?
Resolve gaps with authorized customer/engineering roles.
Value stream
Actual route, information release, queues, holds, and shipment.
Where does elapsed time accumulate and why?
Verify the largest delay with operators and timestamps.
Flow
Batch size, cycle, setup, transfer and acceptance controls.
Can the next accepted unit move without adding risk?
Test one approved sequence or batch change.
Pull
Consumption signal, replenishment time, stock status, pack size.
Can the supplying process reliably respond to actual use?
Pilot only for a stable item with an exception route.
Improvement
Baseline and after data, adverse effects, owner and review date.
Did the change help the customer under the same conditions?
Adopt, adjust, or stop and document the decision.
When the principles need a different application
One-piece flow may not suit a process with physical batch constraints, long cure time, shared equipment, or variable engineering routes. Pull may be premature when actual consumption or supplier lead time is unknown. Value-stream mapping may be too broad for a narrowly defined task problem, while a single-process map may miss a system-level queue. Choose the scale and method to match the decision.
Respect machine safety, qualified-process requirements, inspection controls, customer specifications, and supplier agreements throughout. A future-state map is a proposal until an authorized owner approves and tests it. A local capacity improvement may shift waiting downstream; review order delivery and quality for the full route before claiming success.
Assign an owner at each principle-to-process handoff
The five principles connect work across functions, so record who owns the evidence and who can authorize a change. The customer requirement owner confirms acceptance and delivery; the value-stream owner validates the route and information flow; work-center operators demonstrate the actual sequence; quality controls acceptance and disposition; production control manages order release and priority; purchasing or supplier quality coordinates outside supply. One person can hold several roles in a small shop, but the responsibilities still need to be clear.
Use a handoff review when the order moves from engineering release to planning, from one work center to another, and from outside coating to final inspection. At each point, the sender confirms job and revision, quantity, status, and required record; the receiver acknowledges readiness or raises a gap. A missing handoff is a process issue to resolve, not an invitation to move the job based on a verbal assumption.
Validate demand, flow, and the proposed WIP test
Takt is calculated from available production time and customer demand over the same period. If demand is 10 units per production day and the site has 450 minutes under its stated calendar rule, the 45-minute takt gives a pace reference. It does not account for every setup, shared resource, shift difference, or process qualification. Compare it with capacity by product family and check whether the limiting step can meet the required mix, not just the average.
Before reducing WIP, list the release rule and upstream response. If a queue is at its proposed cap, the planner needs a visible signal to stop release or route a priority exception. If the process is starved, identify whether the cause is missing material, an engineering hold, equipment downtime, or an unrealistic cap. Keep a daily exception log for the test so that the team can tell whether a smaller queue improved delivery or merely moved waiting to another location.
At the review, compare order lead time, late orders, WIP age, first-pass acceptance, and expedites for the same family and time period. Record changed demand and product mix. If throughput falls or late orders rise, do not call the lower WIP a success without explaining the whole customer effect. Use the evidence to revise the rule, return to the previous approved state, or extend the test with a clear hypothesis.
Keep the improvement claim proportional to the evidence
A single fictional order helps explain a method but cannot establish a company result. A real case claim needs a named source, scope, baseline, comparison period, measure definition, and attribution limits. If the team only knows that a change happened before an outcome, describe the sequence without claiming the change caused the outcome. Report operational measures separately from cost or revenue claims.
Retain the map and order review as working records under site policy. Update the future state when validated work changes, remove obsolete versions from the point of use, and identify the next review owner. The repeated cycle should help the team learn from actual customer orders and make the next decision visible.